

Home / CNC-Machining / CNC Milling / CNC Machined Black Anodized Aluminum Bracket Set
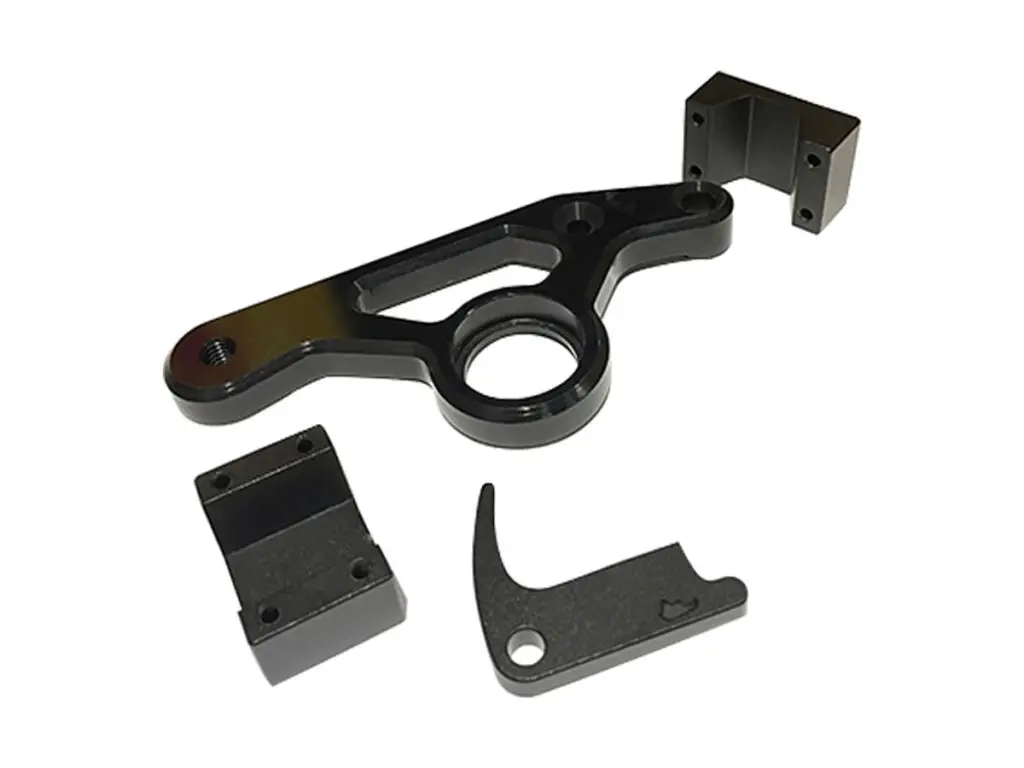
CNC machined black anodized aluminum bracket set, three pieces with matching holes

CNC Machined Black Anodized Aluminum Bracket Set

Bracket sets machined from 6061-T6 plate, supplied as a matched three-piece kit with hole positions within 0.05 mm, machined bend radii instead of formed corners, 0.4 mm edge breaks and a matt black anodized finish. Each piece is marked 1/2/3 and packed as a set.

*Send the assembly drawing rather than the individual parts. The holes only matter relative to each other, and quoting from three separate drawings usually produces a kit that bolts together but does not line up with the frame.

Anodized Bracket Set Overview

A bracket kit is a small assembly pretending to be three parts. Its quality is decided by how the pieces fit each other, not by how each one looks on its own, which is why the set is machined and checked as a group.

The plate is faced, all three profiles are nested and milled from one programme, the holes and threads are cut in the same set-up, then the pieces are anodized in one dye lot so the black matches across the kit.

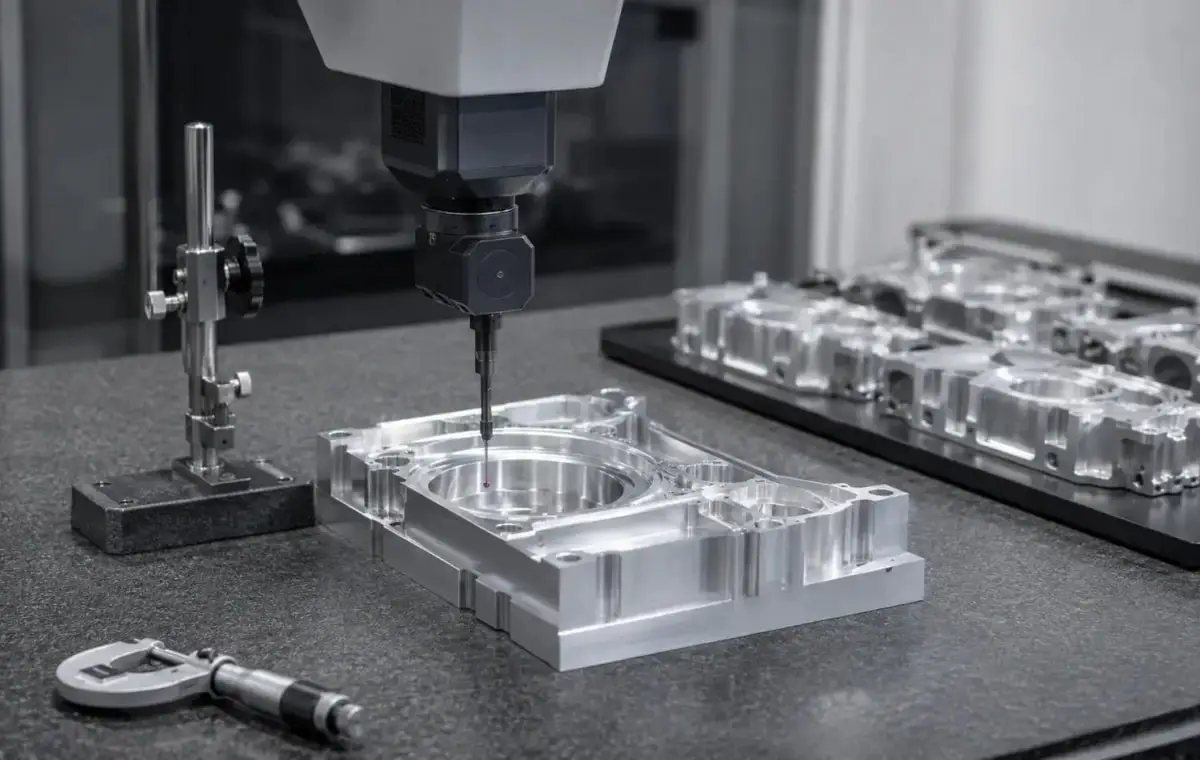
CMM inspection of a gripper jaw set, a brass manifold block and an eight-lobe flange plate
6061-T6 aluminium flat plate stock for CNC milling

6061-T6 Aluminium Plate

6061-T6 is used because the brackets are 6 mm plate with milled radii, and it takes a thread in a 6 mm section without pulling out under a normal M5 fixing load.

7075-T6 aluminium billet block stock for CNC milling

5052-H32 or 6082-T6

5052 is chosen when the bracket has to be formed after machining, since it will not crack at a tight bend. 6082-T6 is used where the kit is welded into a frame and then re-anodized.

Formed brackets and machined brackets are not interchangeable: a formed corner springs back and the hole moves 0.2 mm, which is why this kit has milled radii.

Anodized Bracket Set Specifications

Milling data for a three-piece kit, with the hole, thread and match values that decide whether it assembles first time.

SpecificationMachining DataSpecificationMachining Data
ProductBracket Set / Mounting Kit, 3 PiecesMachining Process3-Axis CNC Milling, Profiling, Tapping
Material6061-T6 Aluminium PlateEnvelopeUp to 180 × 90 × 25 mm per Piece
Plate Thickness5 – 12 mmHole Position±0.05 mm From the Datum Face
Bend RadiusR8 – R20 Machined, Not FormedEdge Break0.4 mm, All Round
ThreadsM3 – M8, Class 6H, 1.5 × D DeepCounterboresDepth ±0.05 mm
Flatness0.05 mm on the Mating FacesSquareness0.05 mm per 50 mm
Set MatchPieces Marked 1/2/3, InterchangeableWeight80 – 420 g per Piece
CustomizationSlot Length, Cable Tie Holes, Logo Engraving, Kit BagLead Time4 – 6 Days Sample, 10 – 14 Days Batch
InspectionCMM Hole Pattern, Thread Gauges, Anodizing ThicknessPackingKit Bag, Foam Divider, Labelled Box

Key Features of Our Bracket Sets

Nested from one plate, matched as a set, anodized in a single dye lot.

Machined as a Matched Set

All three pieces come off one programme with a common datum, so the holes line up when the kit is assembled instead of needing a file at the bench.

Milled Radii, Not Formed Corners

The outside radii are cut, not bent, which keeps the profile within 0.05 mm and avoids the spring-back that moves a formed hole off position.

Threads Cut Before Coating

Threads are tapped to a pre-plate size, then masked during anodizing, so an M5 screw runs in by hand without chasing the thread afterwards.

One Dye Lot for the Kit

All three pieces are anodized together, because black anodizing varies visibly between loads and a kit with two shades looks like it came from two suppliers.

Bracket kit that has to assemble first time?

Surface Finishes for Bracket Sets

The finish is mostly cosmetic, but threads and earth points are functional and cannot take the full coating.

FinishMain PurposeFinishMain Purpose
Black AnodizingMatt black that hides handling marksClear AnodizingKeeps the machined aluminium look
Bead BlastingEven matte before dyeHard AnodizingWear surface on a sliding bracket
Masked ThreadsThreads stay at 6H after coatingLaser MarkingPiece number 1/2/3 and kit code
Anodizing Build10 – 15 µm, SealedChromate ConversionConductive contact for earthing
Edge SealingStops dye pooling at the radiusAssembly GreaseNone, Dry Fit Only
Colour BatchOne Dye Lot per KitScratch TestPencil Hardness 4H Minimum

*Anodizing adds 10 to 15 µm and closes an M5 thread enough to bind a screw. Threads are plugged, and any earth point is masked so the resistance stays under 0.1 ohm.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
All three pieces bolted together on the bench without a file, exactly as they should.

Industrial Components Buyer
The black matches across the set, which was the problem with our previous supplier.

Equipment Manufacturer
The threads took the screws by hand, no chasing needed.

OEM Customer
OEM Customer
A year on the machine frame and the anodizing has not rubbed through at the joints.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.
Trusted for Precision CNC Milling.

Machining Process for Bracket Sets

All three pieces are cut from one plate and one programme, so the set goes together on the machine table before it ever reaches the customer.

01. Assembly Review

Check how the three pieces fit together, confirm the fixing centres and decide the plate thickness from the load the kit carries.

02. Face and Nest the Plate

Face the plate to thickness, then nest all three profiles on one blank so they share a datum and the grain direction.

03. Mill Profiles and Radii

Mill the outside profiles with a 6 mm cutter, leaving the radii as drawn rather than forming them, and check the set against the drawing.

04. Drill, Tap, Counterbore

Drill the fixing holes and counterbores from the same datum, tap the threads and break every edge before the parts leave the machine.

05. Anodize and Kit

Bead blast, anodize black in one load, mask the threads, then mark 1/2/3 and pack the set with a foam divider.

Send the assembly drawing and the fixing centres, and we will quote a matched kit anodized in one lot.

Anodized Bracket Set FAQs

Yes, but the price per piece is higher and the match is not guaranteed, since a single piece may come from a different anodizing load and the black will not be identical.

A formed 6 mm corner springs back by 1 to 2° and moves the hole 0.2 mm, which is enough to stop a kit going together. Milled radii hold 0.05 mm and look sharper.

M3 to M5 through, and M6 with a 1.5 × D depth. Anything deeper needs a thicker plate or a welded boss, because a thread in 6 mm plate has only four full turns.

Standard anodizing is not UV stable and greys within two summers. For outdoor kits we use a sealed anodize plus a clear top coat, or powder coating at 60 to 80 µm.

Yes, laser marking 1/2/3 and the kit code on a face that is hidden in assembly, applied after anodizing so the mark stays legible.

Each set in a labelled bag with a foam divider so the anodized faces do not rub, then boxed. Kits for production lines can be packed in sequence by assembly station.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

CNC turned 17-4PH stainless flanged spindles with ground bearing journals, a square flange face and a threaded nose, held to.

Five-axis CNC machined 7075-T6 aluminium cradle brackets with swept arms, angled mounting pads and lightening pockets, machined.

CNC machined 6061-T6 aluminium angle mounting blocks with two square faces, dowel holes to H7 and drilled fixing patterns, square.

CNC machined 6061-T6 aluminium clevis blocks with two parallel bores held to H7, bore-to-bore parallelism 0.02 mm and a flat.

CNC turned 6061-T6 aluminium bearing ring flanges with a bored bearing seat to H7, bolt circle to ±0.03 mm, faces flat to 0.02 mm.

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top