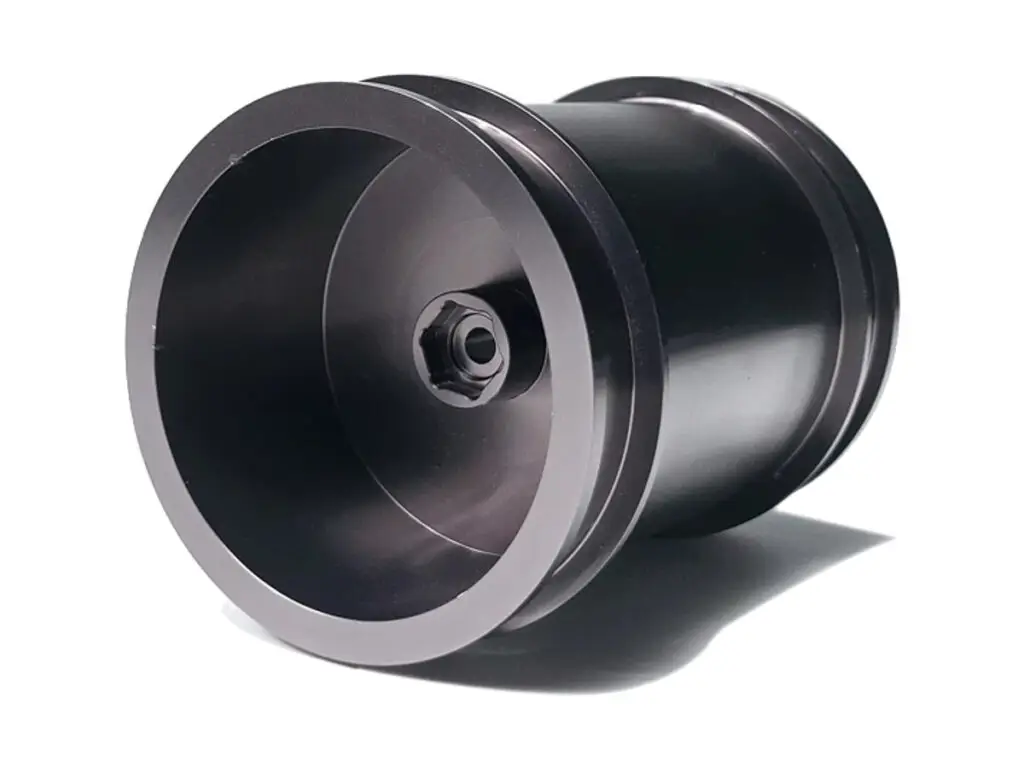


CNC Turned Aluminum V-Belt Pulley
V-belt pulleys turned from 6061-T6 bar, with a groove profile held to ±0.05 mm on angle and depth, groove pitch to ±0.03 mm, bore ground to H7, radial runout of 0.03 mm on the flanks and residual unbalance to G6.3 at 3,000 rpm. Keyways are cut after boring and the rim is balanced before anodizing.
- V-Groove Profile ±0.05 mm
- Bore Ground to H7
- Rim Balanced at Speed
- Keyway Cut After Boring
*Send the belt section and the shaft diameter. The groove angle changes with the belt section, and a pulley cut for an A section will not hold a B belt at the right depth.
V-Belt Pulley Overview
A V-belt pulley transmits torque through friction on two flanks, so the groove angle, the groove depth and the pitch diameter all have to be right. A groove that is too deep lets the belt bottom out and slip; too shallow and the belt rides high and wears.
The pulley is turned from bar or plate, the groove is cut with a form tool and checked with a profile gauge, then the bore is bored and ground. Keyways are cut after boring so the broach does not distort the bore, and the part is balanced before coating.
6061-T6 Aluminium Bar
6061-T6 is the usual choice for light-duty pulleys because it is strong enough for the rim speed, machines to a clean groove and anodizes hard enough to resist belt wear. It also keeps the inertia low on start-stop drives.
7075-T6 or Cast Iron
7075-T6 is used on high-speed or high-torque drives where the rim must not grow. Cast iron is specified where the pulley is a wear part and the belt runs continuously, because it holds the groove profile far longer.
Aluminium suits drives under about 15 kW and intermittent duty; above that, cast iron or steel is cheaper over the life of the groove.
V-Belt Pulley Specifications
Turning data for V-groove pulleys, with the groove, bore and balance values that decide whether the belt runs true.
| Specification | Machining Data | Specification | Machining Data |
|---|---|---|---|
| Product | V-Belt Pulley / Single and Multi-Groove | Machining Process | CNC Turning, Grooving, Boring, Balancing |
| Material | 6061-T6 Aluminium Bar | Diameter Range | Ø 60 – 400 mm |
| Bore | Ø 10 – 80 mm, H7, Ground | Groove Profile | ±0.05 mm on Angle and Depth |
| Groove Pitch | ±0.03 mm Between Grooves | Radial Runout | 0.03 mm on the Groove Flanks |
| Axial Runout | 0.02 mm on the Rim Face | Balance | G6.3 at 3,000 rpm |
| Keyway | Width ±0.02 mm, Depth ±0.05 mm | Wall Thickness | 6 – 20 mm at the Hub |
| Customization | Taper Lock Bush, Split Hub, Lightening Holes | Lead Time | 5 – 7 Days Sample, 12 – 16 Days Batch |
| Inspection | Groove Profile Gauge, Bore Air Gauge, Runout Between Centres, Balance Report | Packing | Foam Ring, Individually Boxed, Crate |
Key Features of Our V-Belt Pulleys
Groove gauged, bore ground, rim balanced.
Groove Checked With a Profile Gauge
Every groove is checked against the belt section gauge, so the belt sits at the correct depth and does not bottom out under load.
Bore Ground to H7
The bore is ground rather than reamed, which holds the fit and the concentricity that keeps the pulley from running out at speed.
Keyway Cut After Boring
Broaching a keyway distorts the bore, so the keyway is cut last and the bore is checked again before the pulley is balanced.
Balanced Before Coating
The rim is balanced by removing material from the inside face, not the groove, and the balance mark is transferred to the finished part.
Pulley that has to run without vibration?
Surface Finishes for V-Belt Pulleys
The groove flanks are the working surface; the bore and keyway are fits; the rest is cosmetic.
| Finish | Main Purpose | Finish | Main Purpose |
|---|---|---|---|
| Type II Anodizing | Corrosion protection and colour coding | Hard Anodizing | Wear resistance in the V-groove |
| Masked Bore and Keyway | Keeps the shaft fit at H7 | Bead Blasting | Even matte before dye |
| Laser Marking | Pulley size and balance mark | Bare Groove Flanks | Uses the aluminium surface as the belt running face |
*Hard anodizing in the groove raises the surface by 25 to 50 µm and changes the effective pitch diameter. Grooves can be masked, or machined undersize and finished after coating.
Put your CNC milling parts into production today
All information and uploads are secure and confidential.
Trusted for Precision CNC Machined Components
Supporting OEM projects with accurate machining, flexible production, and reliable component quality.
Trusted for Precision CNC Milling.
Turning Process for V-Belt Pulleys
The V-groove is turned and checked with a profile gauge before the bore is finished, so the belt sits at the right depth instead of bottoming out.
01. Belt and Shaft Review
Confirm the belt section, the number of grooves and the shaft fit, then choose the groove tool and the bore allowance.
02. Turn the Blank
Face, centre and turn the outside diameter and both faces, leaving 0.3 mm on the groove flanks and 0.2 mm in the bore.
03. Cut the Grooves
Cut each groove with a form tool at constant feed, check the profile with a gauge and measure the pitch between grooves before parting off.
04. Bore, Keyway and Balance
Bore and grind the bore to H7, cut the keyway, then balance the pulley and mark the correction position on the rim.
05. Anodize and Inspect
Mask the bore and keyway, anodize, then check runout between centres and record the balance before packing each pulley in foam.
Send the belt section and the shaft diameter, and we will quote a pulley with the groove gauged and the bore ground to H7.
V-Belt Pulley FAQs
Yes, any angle from 34° to 40° held to ±0.05°, machined with a form tool ground to the angle. The gauge is made to the same angle so the check is meaningful.
Because at 3,000 rpm a 300 mm pulley with 20 g of unbalance produces enough force to wear the bearing. Balancing removes material from the inside face, away from the groove.
Yes, by 5 to 10 µm per surface in Type II and 25 to 50 µm in hard anodizing. Grooves that must stay on size are masked, or the pulley is machined undersize and finished after coating.
Yes, the hub is bored and machined to the bush drawing, with the split and the screw holes positioned so the bush pulls the pulley onto the shaft squarely.
The bore is machined in the same set-up as the groove, or ground between centres afterwards, holding concentricity to 0.02 mm so the belt does not run out of line.
400 mm diameter. Above that the pulley is machined as a rim and a hub, then bolted and dowelled, which keeps the groove accurate but adds a joint.
Other CNC Machined Mechanical Components
Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.
Custom CNC machined aluminium cavity bases for automation and electronic equipment.
Explore CNC milled clutch levers in 6061 or 7075 aluminum, built for smooth pivot movement, accurate fit, comfortable control,.
Custom CNC machining milling aluminum engine brackets with 6061/7075 aluminum, complex milling, multiple finishes and precision.
CNC milled aluminium servo motor mounting bases with a bored pilot register, face flat to 0.02 mm and shaft centre height held to.
Custom CNC machined steel hydraulic manifold blocks with cross-drilled galleries and gauged ports.
Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!