
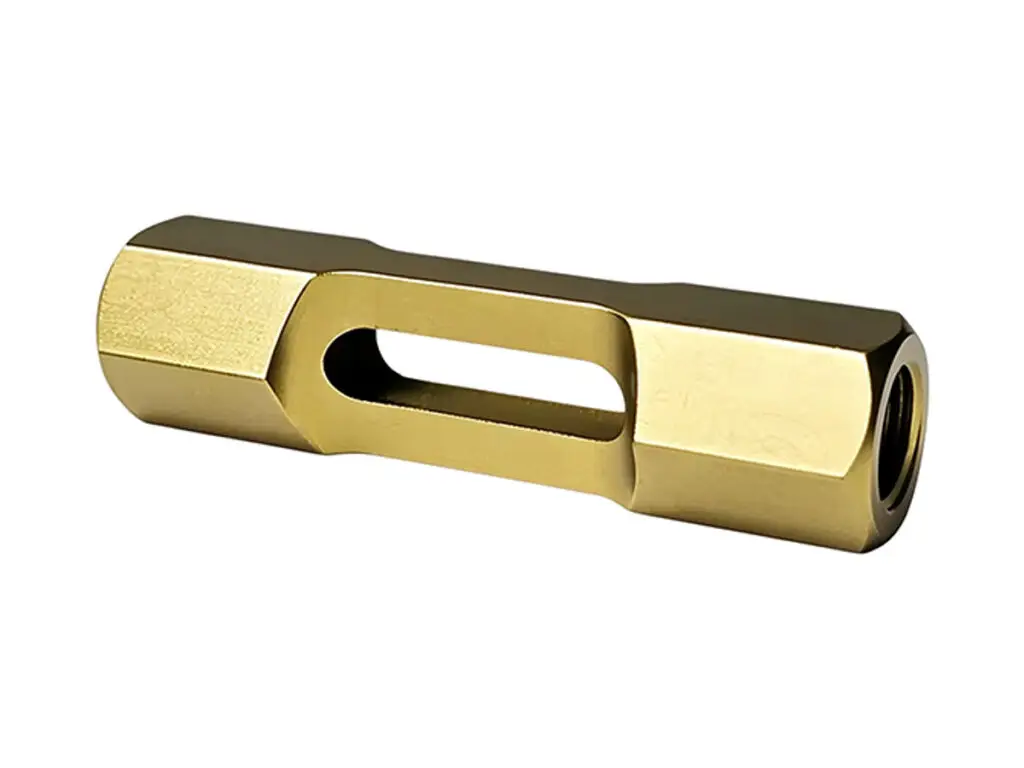


CNC Turned Brass Extended Coupling Nut
Coupling nuts turned from C36000 brass, with a through thread from M4 to M16 held to class 6H, hex flats within 0.05 mm, ends square to the thread axis within 0.03 mm and a chamfer at both ends. Threads are plug gauged from either end before packing.
- Through Thread to 6H
- Hex Flats Within 0.05 mm
- Ends Square to 0.03 mm
- Thread Gauged Both Ends
*Tell us the stud length and whether the nut has to bottom on a shoulder. A through thread that is not gauged from both ends will take a stud 20 mm in and then bind, which is the most common complaint on long coupling nuts.
Brass Coupling Nut Overview
A coupling nut is a long hex with a thread all the way through, used to join two studs or to stand a component off a panel. Its two failure modes are a thread that is not straight and an end that is not square, both of which show up as a stud that will not run in.
Bar is turned to the hex across flats, faced, centre drilled and threaded from both ends with a machine tap on a floating holder, then the second end is faced square and chamfered before gauging.
C36000 Free-Cutting Brass
C36000 machines at high speed with a clean chip and leaves a thread flank that gauges consistently, which matters on a through thread where the tap has to run 60 mm without wander.
C37700 or 304 Stainless
C37700 is used where the nut is hot forged and then threaded for a heavier section. 304 is chosen for wet or marine assemblies, where brass dezincifies and the nut seizes on a stainless stud.
A brass nut on a stainless stud needs anti-seize; without it the two gall and the nut is cut off rather than unscrewed.
Brass Coupling Nut Specifications
Turning and threading data for extended nuts, with the thread, hex and squareness values that decide whether a stud runs in cleanly.
| Specification | Machining Data | Specification | Machining Data |
|---|---|---|---|
| Product | Extended Coupling Nut / Threaded Spacer | Machining Process | CNC Turning, Thread Milling, Hex Milling |
| Material | C36000 Free-Cutting Brass | Envelope | M4 – M16, Length 15 – 80 mm |
| Thread | Through, Class 6H, Metric or UNC | Thread Depth | Full Length, Chamfered Both Ends |
| Hex Across Flats | 8 – 24 mm, ±0.05 mm | Across Corners | ±0.08 mm |
| End Squareness | 0.03 mm to the Thread Axis | Concentricity | Thread to Hex Within 0.05 mm |
| Chamfer | 0.5 × 45° Both Ends | Surface Finish | Ra 1.6 µm, Nickel on Request |
| Length Tolerance | ±0.10 mm | Bore Coaxiality | 0.04 mm for a Shoulder Nut |
| Customization | Left Hand Thread, Shoulder, Knurl, Cross Hole, Slot | Lead Time | 3 – 5 Days Sample, 8 – 12 Days Batch |
| Inspection | Thread Plug Gauge Both Ends, Hex Micrometer, Squareness Bench | Packing | Bulk Bag, Then Boxed by Size |
Key Features of Our Coupling Nuts
Threaded and gauged from both ends, hex held within 0.05 mm, ends square.
Thread Gauged From Both Ends
A long through thread is checked with a plug gauge at each end, because a tap that wanders shows only at the far end and a nut that passes one way can still bind the other.
Hex Milled After Turning
The hex is milled on a second operation from the thread axis, holding flats within 0.05 mm so a spanner sits flat and does not round the corners under load.
Ends Faced Square
Both ends are faced after threading to 0.03 mm squareness, so the nut seats flat against a panel and does not load the thread with a bending moment.
Chamfer at Every Entry
A 0.5 mm chamfer at both ends guides the stud in and removes the burr that a tap leaves when it breaks out of the last thread.
Coupling nut that has to run on freely?
Surface Finishes for Coupling Nuts
The thread is the function, the hex is the interface and the outside is cosmetic, so plating thickness has to be controlled.
| Finish | Main Purpose | Finish | Main Purpose |
|---|---|---|---|
| Natural Brass | Conductive and solderable as machined | Nickel Plating | Wear resistance on a repeatedly used nut |
| Clear Lacquer | Stops tarnish in storage | Tin Plating | Solderable and RoHS compliant |
| Bead Blasting | Matte decorative finish | Passivation | Removes machining residue before plating |
| Plating Build | 3 – 8 µm, Threads Masked or Re-tapped | Ultrasonic Clean | Before Packing |
| Anti-Seize | Applied on Request | Thread Protector | Plastic Cap Both Ends |
| Colour Match | Nickel Satin or Bright | Salt Spray | 96 h on Nickel |
*Nickel at 8 µm closes a 6H thread by 16 µm on the flanks. Long nuts are either masked at the thread or re-tapped after plating, and every one is gauged again before packing.
Put your CNC milling parts into production today
All information and uploads are secure and confidential.
Trusted for Precision CNC Machined Components
Supporting OEM projects with accurate machining, flexible production, and reliable component quality.
Trusted for Precision CNC Milling.
Machining Process for Coupling Nuts
The thread is cut through in one pass and gauged from both ends, so a coupling nut joins two studs without bottoming out halfway along.
01. Stud and Thread Review
Check the stud length, the thread class and whether the nut bottoms on a shoulder, then set the blank length with facing allowance.
02. Turn and Face the Blank
Turn the outside diameter, face the first end square and centre drill, keeping the bar in the collet for the threading pass.
03. Thread From Both Ends
Tap from each end with a floating holder, clearing chips between passes, until the plug gauge runs through without a tight spot.
04. Mill the Hex
Milled the hex from the thread axis and check across flats with a micrometer at both ends, since a hex that tapers will grip only at one face.
05. Face, Chamfer, Gauge
Face the second end square, chamfer both entries, gauge the thread from each side and clean before plating or bagging.
Send the stud and the thread callout, and we will quote a coupling nut threaded through and gauged from both ends.
Brass Coupling Nut FAQs
Up to 80 mm from M4 to M16. Beyond that the tap wanders, so longer nuts are threaded from both ends and the two threads are clocked to meet in the middle.
Yes, across flats follows the standard metric or imperial series, within 0.05 mm, so a stock spanner fits without rounding the corners.
Yes, one or both ends, cut with a left hand tap and marked LH on the hex flat so the nut cannot be fitted the wrong way round.
It adds about 8 µm per flank. Nuts that must run on by hand are masked at the thread or re-tapped after plating, and every nut is gauged before it is packed.
Yes, a shoulder nut is turned from bar with the collar concentric to the thread within 0.04 mm, which is what stops a panel from sitting at an angle.
±0.10 mm as standard and ±0.05 mm on request. Length matters when the nut sets a panel gap, and a 0.2 mm error shows as a visible step between two panels.
Other CNC Machined Mechanical Components
Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.
CNC machined 7075-T6 aluminium gripper jaws cut as a matched pair, with the grip profile machined to your part, dowel holes to H7.
CNC turned brass slotted bushings with a honed bore, milled lubrication slots and a chamfered lead-in, held to 0.01 mm and.
Five-axis CNC machined aluminium gearbox end caps with a compound-angle boss, a bored bearing seat and cooling fins, machined in.
CNC machined aluminium perforated mounting plates with a lightening hole pattern, edge datum faces and counterbored fixings, flat.
CNC machined 6061-T6 aluminium mounting brackets with a machined mounting face, slotted holes and an even anodized finish, held.
Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!



