

Home / CNC-Machining / CNC Milling / CNC Machined Aluminum Gripper Jaw Set
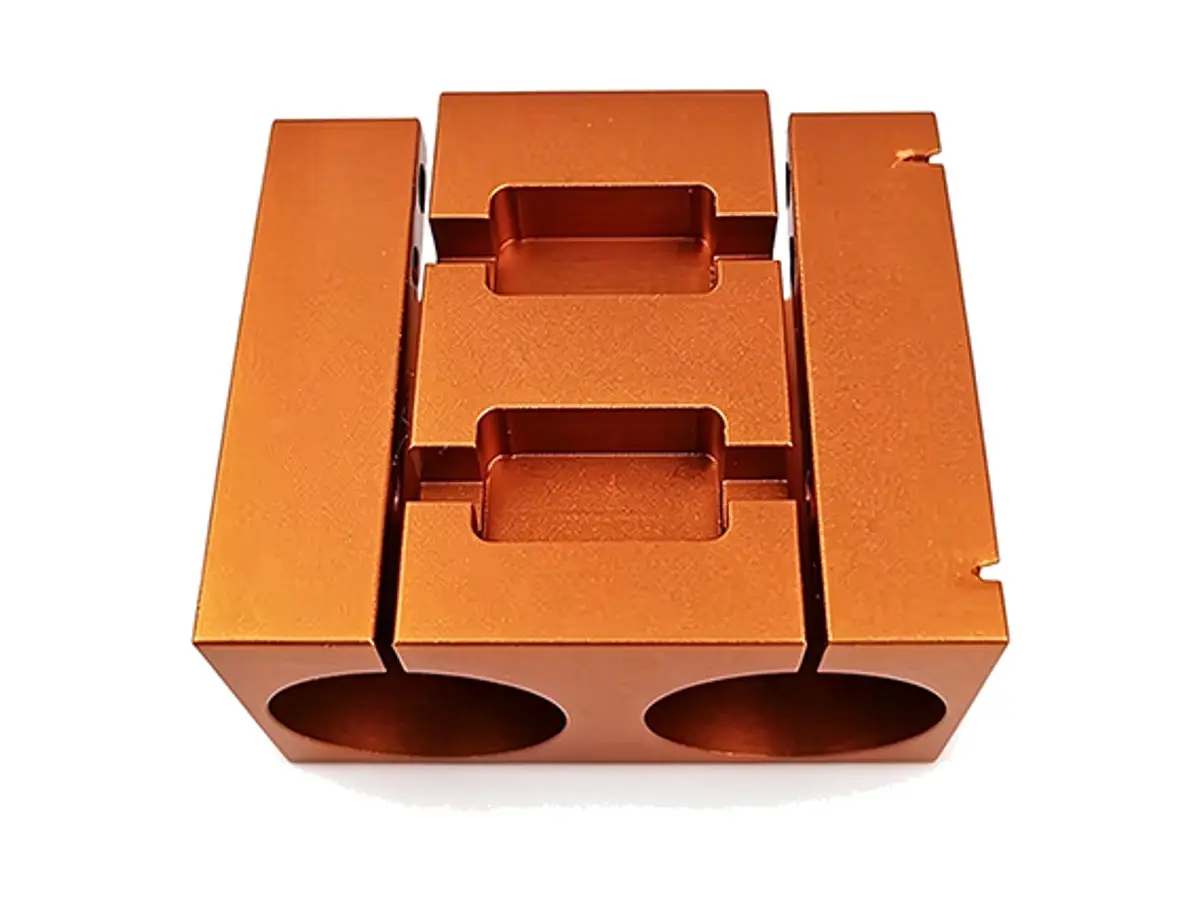
CNC machined anodized aluminum gripper jaw pair with a profiled grip face and dowel holes

CNC Machined Aluminum Gripper Jaw Set

Gripper jaws machined from 7075-T6 as a matched pair, with the grip profile cut to your part model within 0.03 mm, mounting faces flat to 0.02 mm, dowel holes to H7 and the contact face hard anodized with the dowels masked.

*Send the part STEP file and the gripper drawing. The jaw opening and the grip depth come from the gripper stroke, and a profile cut 0.05 mm deep will mark a polished part on every cycle.

Gripper Jaw Set Overview

A jaw pair is a mirror image, and the two halves have to agree: if one profile is 0.05 mm shallow, the gripper pulls the part to one side and the robot repeatability is lost before the jaws wear.

Both jaws are cut from the same billet and programme, the grip profile is finished with a small cutter to follow the part radius, then the pair is measured against each other and the dowels are reamed before anodizing.

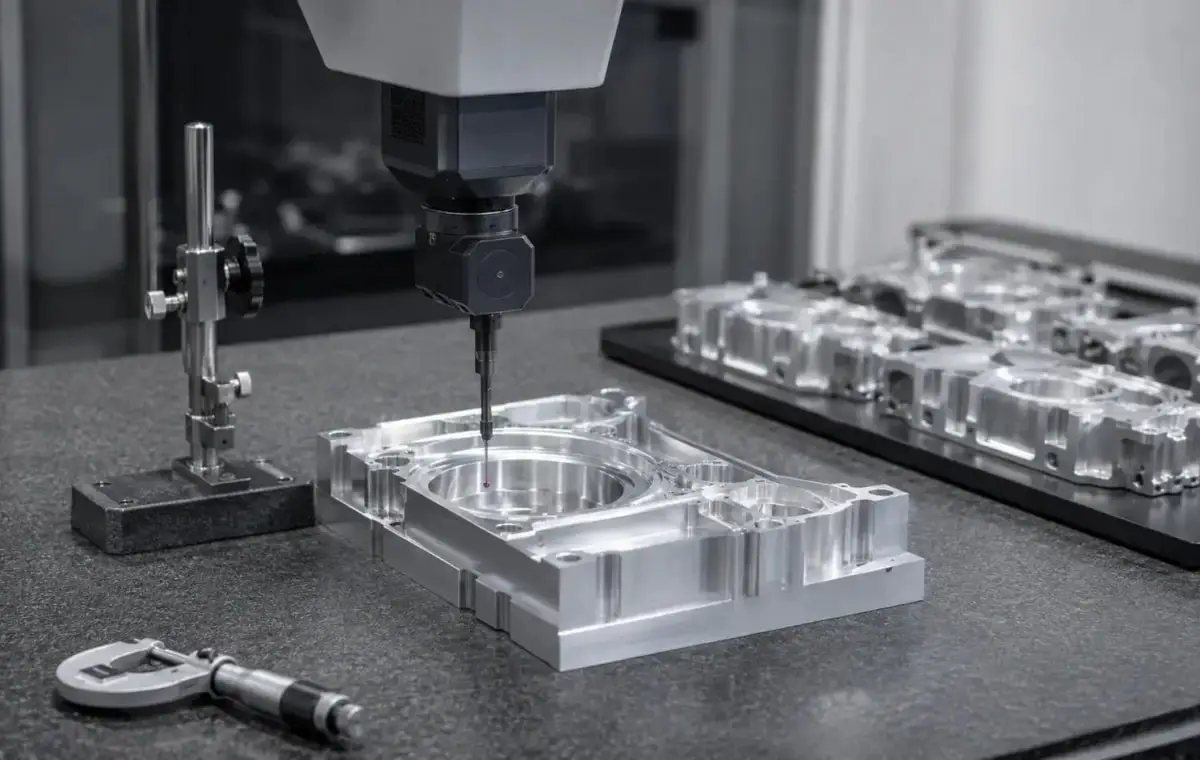
CMM inspection of a gripper jaw set, a brass manifold block and an eight-lobe flange plate
6061-T6 aluminium flat plate stock for CNC milling

7075-T6 Aluminium Block

7075-T6 is used because the jaw section is thin at the grip and has to resist bending every cycle. It also hard anodizes to a surface that does not gall against a machined aluminium part.

7075-T6 aluminium billet block stock for CNC milling

6061-T6 or 6082-T6

6061 is chosen for light-duty jaws on plastic parts, where a softer contact face is an advantage. 6082 is used when the jaws are also the fixture and see cooling fluid every day.

For glass or painted parts, the jaw is machined 0.2 mm under the part profile and a bonded rubber pad takes up the difference; metal-to-metal contact will mark the part.

Gripper Jaw Specifications

Milling data for matched jaw pairs, with the profile, match and dowel values that keep the gripper repeatable.

SpecificationMachining DataSpecificationMachining Data
ProductGripper Jaw / Robot Finger Jaw PairMachining Process3-Axis CNC Milling, Profiling, Boring
Material7075-T6 Aluminium BlockEnvelopeUp to 160 × 80 × 60 mm per Jaw
Grip ProfileMachined to the Part Model, ±0.03 mmPair MatchProfile Match Within 0.02 mm
Jaw Flatness0.02 mm on the Mounting FaceDowel HolesØ 4 – 8 mm, H7
Mounting HolesCounterbored, Position ±0.03 mmJaw OpeningSet by Your Gripper Stroke
Contact FaceSerrated, Smooth or Rubber BondedEdge Break0.5 mm, No Burr on the Grip Face
Jaw HardnessHard Anodized 350 – 450 HVGrip Depth2 – 25 mm, Cut to the Part
CustomizationV-Groove, Radius Nest, Sensor Pocket, Part Ejection SlotLead Time4 – 6 Days Sample, 10 – 14 Days Batch
InspectionProfile Projector, CMM Pair Match, Dowel Pin FitPackingPair Boxed Together, Foam Separated

Key Features of Our Jaw Sets

Cut from one programme, matched to 0.02 mm, masked at the dowels.

Pair Cut From One Programme

Both jaws come off the same toolpath with the mirror applied in CAM, so the grip profile matches within 0.02 mm and the part is not pushed sideways.

Profile Follows Your Part Model

The grip is programmed from the STEP file, not from a nominal radius, which stops point contact on a curved part and the marks that come with it.

Dowel Holes Reamed to H7

Location is by dowels rather than screws, so a jaw can be swapped and the gripper still closes in the same place without re-teaching the robot.

Contact Face Finished Last

The grip face is the last feature cut, after all the mounting work, so it cannot be damaged by clamping or by a drill breaking through.

Jaws that have to grip without marking?

Surface Finishes for Gripper Jaws

The contact face determines grip and marking, the mounting face determines location, and they are finished differently.

FinishMain PurposeFinishMain Purpose
Hard AnodizingWear resistance on the contact faceBlack AnodizingStandard machine finish
Masked Dowel HolesKeeps the H7 location after coatingBead BlastingEven matte before dye
Rubber BondingGrip on glass or painted partsLaser MarkingJaw number and pair serial
Anodizing Build25 – 50 µm on Wear FacesBead BlastBefore Hard Anodizing
Dowel PlugsRemoved After CoatingPair SerialMarked Inside the Mounting Pocket
Assembly GreaseLight Film on the Mounting FaceProtective WrapPer Jaw, Pair Boxed

*Hard anodizing builds 25 to 50 µm and will close a H7 dowel hole. Dowels are masked with plugs, and the grip profile is checked again after coating because the build is not uniform on a radius.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
Both jaws grip at the same time now, and the parts stopped shifting in the gripper.

Industrial Components Buyer
The dowels went in with a light press, and a jaw swap does not need a re-teach.

Equipment Manufacturer
No marks on the anodized parts after a full month of running.

OEM Customer
OEM Customer
The profile was right first time from the model, with no hand fitting at all.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.
Trusted for Precision CNC Milling.

Machining Process for Gripper Jaws

Both jaws are cut from the same programme and checked against each other, so the grip closes on the part evenly instead of pinching one corner.

01. Part and Gripper Review

Check the part model, the gripper stroke and the mounting pattern, then decide the grip depth and whether a rubber pad is needed.

02. Machine the Mounting Side

Face and machine the mounting face, dowel holes and counterbores first, because everything else is located from that face.

03. Rough the Grip Profile

Rough the grip with a 6 mm cutter leaving 0.3 mm, then semi-finish so the finishing cutter sees an even load around the radius.

04. Finish and Match the Pair

Finish the profile with a 3 mm cutter, measure the pair against each other on the CMM and correct any difference over 0.02 mm.

05. Anodize and Re-check

Mask the dowels, hard anodize the contact face, then re-check the profile and the dowel fit before the pair is boxed.

Send the part STEP file and the gripper mounting drawing, and we will quote a matched jaw pair with the grip cut to your part.

Gripper Jaw FAQs

0.02 mm on the grip profile, measured against each other rather than against nominal. That is what keeps the part centred instead of being pushed to the fixed jaw.

Yes, from a scanned point cloud or a STEP model. Cast parts vary by up to 0.8 mm, so the jaw is usually cut to the nominal model with a 0.3 mm relief where the casting is inconsistent.

It adds 25 to 50 µm per surface, which tightens the grip by that amount. Jaws for precision parts are machined undersize, coated and then finished, or the dowels are masked and the profile is left uncoated.

A bonded rubber or PU pad, or a larger contact radius. Metal on metal at 0.5 MPa contact pressure leaves a mark on anodized aluminium within a few thousand cycles.

Yes, a pocket for a proximity or Hall sensor with a 0.5 mm wall is machined in the same set-up. The pocket is kept out of the grip zone so swarf cannot collect in it.

About 500,000 cycles on a clean aluminium part with hard anodized faces, and about 150,000 on a cast part with sand still on it. The dowels usually outlast the grip face.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

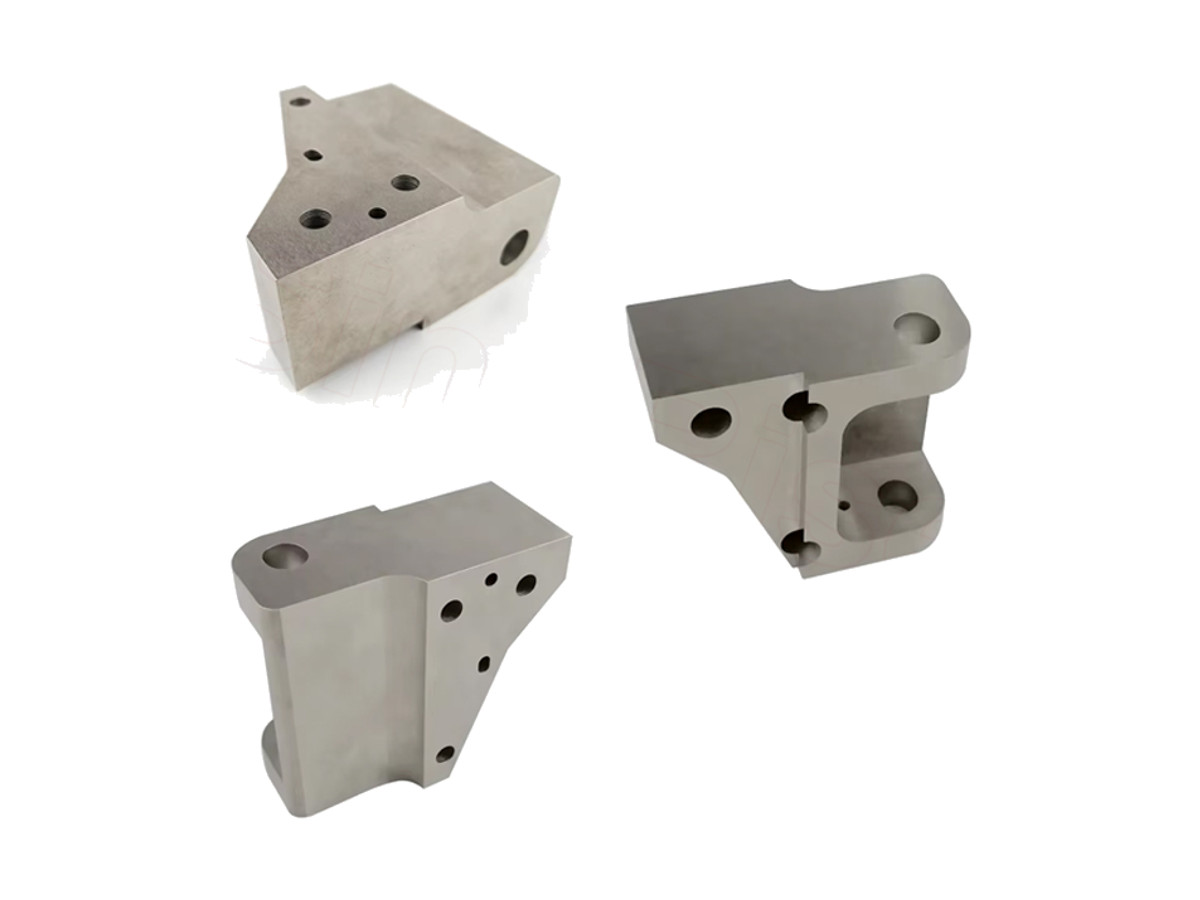
CNC machined 6061-T6 aluminium angle mounting blocks with two square faces, dowel holes to H7 and drilled fixing patterns, square.

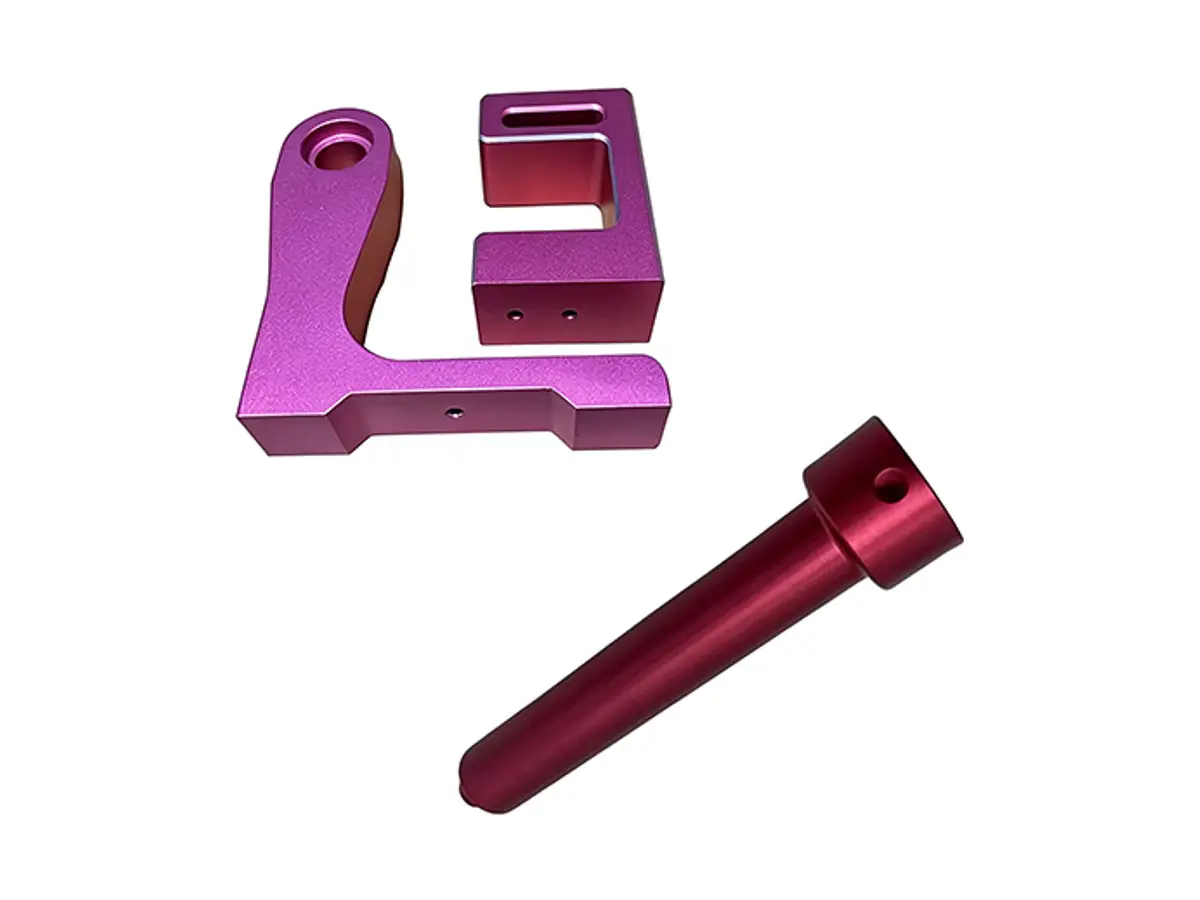
CNC machined aluminium joint bracket and clamping blocks with a split bore, matched hinge pin and anodized finish for robot.

CNC milled aluminium split clamping blocks with a sawn split, matched halves and bores held to H7 for linear shafts.

Custom five-axis CNC machined stainless steel turbine stators and nozzle rings.

Precision CNC machined stainless steel gripper fingers for robot end effectors.

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top