Home / CNC-Machining / CNC-Turning / CNC Turned Stainless Steel Mounting Disc
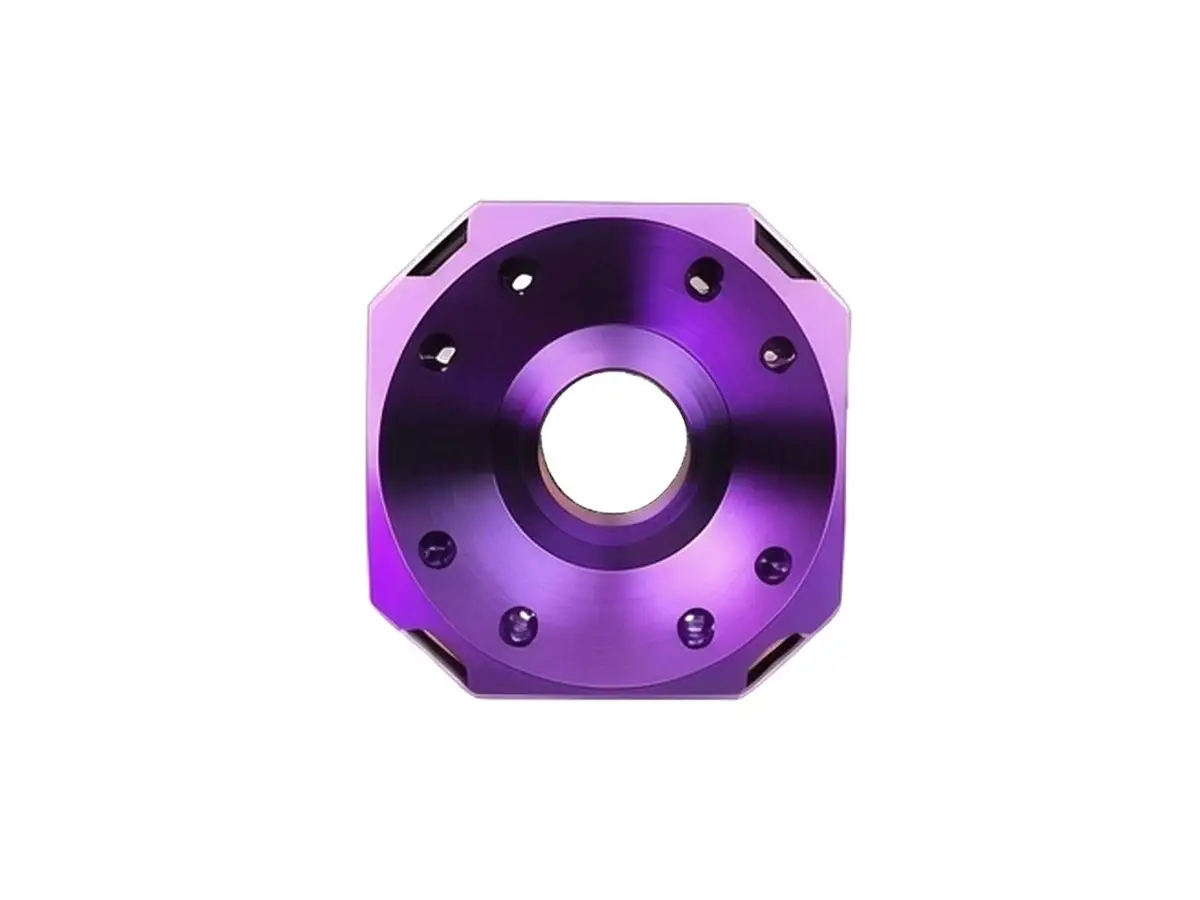
CNC turned stainless steel mounting disc with a recessed centre and a four hole bolt pattern

CNC Turned Stainless Steel Mounting Disc

304 and 316L stainless mounting discs turned from bar with faces flat and parallel to 0.02 mm, a recessed centre machined to depth, three to eight bolt holes on a pitch circle within 0.03 mm and an outside diameter turned as a locating register. Passivated after drilling so the holes do not start to pit.

*Tell us which face is the datum. A disc with a recess on one side and a register on the other has to be machined in a known order, and guessing that order is how a batch ends up 0.1 mm thick on one side.

Stainless Mounting Disc Overview

A disc like this clamps or centres something: a bearing, a hub, a sight glass or a flange cover. Its job is to sit flat, hold a bolt pattern and present a true outside diameter, and all three come from how it is held while it is turned.

The blank is faced on one side, flipped onto a soft jaw that has been bored to the diameter, and faced again, so both faces are parallel to the same axis. The recess and the bolt circle are then cut from the second face, and every hole is deburred on both sides before passivation.

CNC turning of a brass threaded flange bushing, an aluminum bearing sleeve and a retaining cover disc
304L stainless steel round bar stock for CNC machining

304 Stainless Bar

304 is used for a disc that sees washdown or outdoor service but no chlorides: it machines predictably, takes a clean passivated finish and is cheaper than 316L at the same thickness.

304L stainless steel plate and block stock for CNC machining

316L for Chloride Service

316L is specified where the disc sits in salt water, brine or chlorine-based cleaning, because the molybdenum addition is what stops pitting starting in a drilled hole.

The environment rather than the load decides between 304 and 316L on a disc, since neither is a highly stressed part at these thicknesses.

Stainless Mounting Disc Specifications

Turning and drilling data for stainless discs, with the flatness, thickness and bolt pattern values that decide whether the part seals or clamps.

SpecificationMachining DataSpecificationMachining Data
ProductMounting Disc / Clamp DiscMachining ProcessCNC Turning, Facing, Drilling, Boring
Material304 or 316L Stainless BarDiameter80 – 350 mm
Thickness6 – 40 mmFace Flatness0.02 mm
Parallelism0.02 mm Face to FaceBolt HolesØ 5 – 18 mm, 3 – 8 Holes
Bolt PatternPCD ±0.03 mmCentre RecessØ 30 – 200 mm, Depth ±0.05 mm
Surface FinishRa 1.6 µm FacesPassivationASTM A967
CustomizationKeyway, Tapped Centre, O-Ring Groove, Lightening PocketsLead Time5 – 7 Days Sample, 12 – 15 Days Batch
InspectionGranite Flatness, CMM Bolt Pattern, Micrometer ThicknessPackingFelt Interleaved, Carton, Edge Protected

Key Features of Our Turned Discs

Both faces from one axis, holes deburred through.

Both Faces Turned From One Axis

The disc is flipped into a bored soft jaw rather than re-chucked on the rough edge, so the faces are parallel to 0.02 mm and the disc does not rock when bolted.

Bolt Circle From the Turned OD

The pattern is positioned from the finished outside diameter, which is also the register, so the holes and the register agree within 0.03 mm.

Recess Depth Controlled

The centre recess is cut to depth with a positive stop and checked with a depth micrometer, since the recess sets how far a hub or a glass sits into the disc.

Holes Deburred on Both Sides

Every hole is deburred from both faces by hand, because a burr on the underside holds the disc off its seat and shows up as a leak or a wobble.

Disc that has to sit flat and hold a bolt pattern?

Surface Finishes for Stainless Discs

Stainless discs are usually visible, so the finish is both protective and cosmetic.

FinishMain PurposeFinishMain Purpose
PassivationRemoves free iron after drillingElectropolishingBright hygienic faces for washdown plant
Glass Bead BlastingEven matte finish that hides handling marksMasked BoreBore kept at size where a shaft passes through
Laser MarkingBolt pattern and torque order on the faceUltrasonic CleaningRemoves polishing residue before packing

*Electropolishing removes 5 to 15 µm per face, which matters on a disc where thickness is tolerance-critical. Those discs are machined oversize and measured after polishing.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
The disc sits flat on the flange with no rocking, and the bolts torque down evenly.

Industrial Components Buyer
The bolt pattern lined up with the tapped holes without opening them out.

Equipment Manufacturer
The recess depth was right, so the glass sits flush with the frame.

OEM Customer
OEM Customer
Faces were still flat after passivation, which we check on every batch.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.

Trusted for Precision CNC Milling.

Turning Process for Mounting Discs

Both faces are turned in one clamping, so the disc sits flat on the flange instead of rocking on a high spot.

01. Datum and Bolt Review

Confirm which face is the datum, the recess depth and the bolt pattern, and decide whether thickness is measured before or after passivation.

02. Face the First Side

Hold the blank on the sawn edge, face the first side and turn the outside diameter to a clean circle that the soft jaw can pick up.

03. Flip and Face to Thickness

Bore a soft jaw to the finished diameter, hold the disc on that diameter and face the second side to thickness, leaving the recess for the next pass.

04. Recess and Drill

Cut the centre recess to depth, drill and tap the bolt pattern from the turned OD, then deburr every hole on both faces.

05. Passivate and Check

Ultrasonically clean, passivate, then check flatness on granite, thickness by micrometer and the bolt pattern on the CMM before interleaving with felt.

Send the disc drawing with the face you use as a datum, and we will quote it with flatness and bolt pattern both checked on the finished part.

Stainless Mounting Disc FAQs

0.02 mm on a disc up to 300 mm diameter, checked on granite. Above that the bar is heavier and the second face is turned in two passes, which holds 0.03 mm with a blended step.

Yes, but it takes three operations: face and turn one register, flip on that register, face and cut the second. The two registers are then concentric within 0.03 mm.

By a few micrometres at most, which is inside the usual tolerance. If thickness is critical the disc is measured after passivation, not before.

Up to 350 mm diameter with holes to Ø 18 mm. Larger patterns are drilled on the mill with the disc on a rotary table, which holds the same ±0.03 mm.

Yes, from 1.5 mm wide and 1 mm deep, interpolated in one pass so the groove depth is uniform all the way round.

By hand on both sides. A machine brush rounds the entry but leaves the exit burr, and an exit burr is what holds a disc off its seat.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

Custom CNC machined aluminium drone components, including arm mounts, motor mounts and frame fittings.

Custom CNC machined aluminium robot joint actuator components with concentric threads, sealing faces and hex flats.

Custom CNC machined robot end effector flanges for tool mounting and automation.

Custom Brake Lever CNC Milled components manufactured with precision CNC machining, supporting OEM customization, lightweight.

CNC machined aluminium robot mounting brackets supplied as matched pairs, right-angle held to 0.05 mm, gusseted for stiffness and.

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top