


Home / CNC-Machining / CNC-Turning / CNC Turned Stainless Steel Flanged Bushing Set
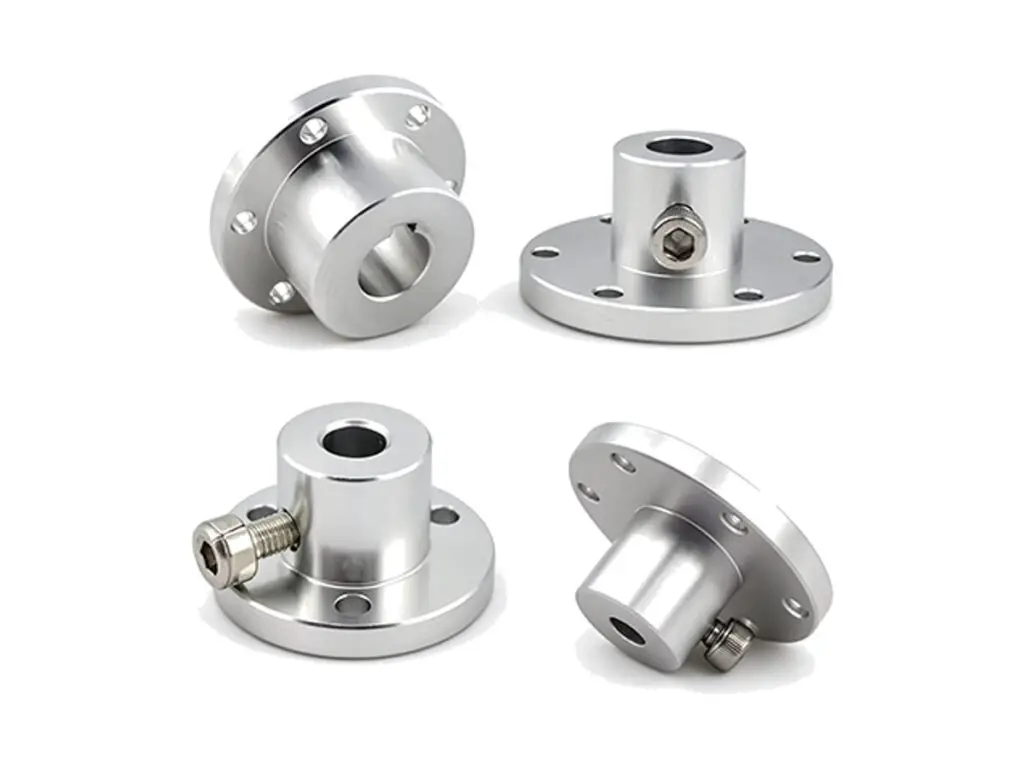
CNC turned stainless steel flanged bushings with an H7 bore and a flange square to the bore

CNC Turned Stainless Steel Flanged Bushing Set

Flanged bushings turned from 304 stainless, with a bore held to H7 and round within 0.01 mm, an outside diameter at m6 for a press fit, a flange square to the bore within 0.02 mm and thickness at ±0.03 mm, supplied as a set matched within 0.05 mm.

*Send the housing bore and the shaft size. A bushing pressed into a housing 0.02 mm over m6 will close its own bore by 0.01 mm, and the shaft that fitted on the bench will not go in after pressing.

Flanged Bushing Set Overview

A flanged bushing carries a shaft and takes axial load on its flange. Pressing it in closes the bore slightly, so the bore has to be sized for the housing, not for the bench.

The bushing is turned and bored in one clamping, the flange is faced square, the outside is turned to m6 and the bore is finished after the press fit allowance is applied.

Assembly and inspection of a rod end clevis, a slotted drive hub and a split clamp ring
304L stainless steel round bar stock for CNC machining

304 Stainless

304 is the default for washdown and outdoor pivots: it does not need a coating, and passivation keeps the bore clean. It galls on a stainless shaft, so the bore is finished finer than a bronze bush.

304L stainless steel plate and block stock for CNC machining

Bronze or 316L

Oil-impregnated bronze is chosen where the bushing runs dry or at low speed, and 316L where chlorides are present and 304 would pit at the flange edge.

A 2.5 mm wall is the minimum for a press fit; thinner than that the bore closes 0.02 mm when the bushing is pressed and the shaft seizes.

Flanged Bushing Specifications

Turning and boring data for press-fit bushings, with the bore, flange and set values that keep a shaft turning freely.

SpecificationMachining DataSpecificationMachining Data
ProductFlanged Bushing Set (2 – 6 Pieces)Machining ProcessCNC Turning, Boring, Flange Facing
Material304 Stainless, 316L or Bronze on RequestEnvelopeBore Ø 8 – 50 mm, Flange Ø 16 – 70 mm
BoreH7, Roundness 0.01 mmBore FinishRa 0.8 µm, Ra 0.4 µm Honed
FlangeSquare to the Bore Within 0.02 mmFlange Thickness±0.03 mm
Outside Diameterm6 for a press fit, ±0.01 mmWall Thickness2.5 mm Minimum
Length±0.05 mm, Set Within 0.05 mmOil GrooveWidth ±0.05 mm, Depth ±0.03 mm
Weight10 – 180 g per PieceCoatingPassivated, No Coating in the Bore
CustomizationFlange Diameter, Oil Groove, Cross Hole, Set QuantityLead Time5 – 7 Days Sample, 12 – 16 Days Batch
InspectionBore Air Gauge, Flange Squareness on Granite, Set Match CheckPackingBore Plug, Bagged by Set

Key Features of Our Flanged Bushings

Flange and bore from one clamping, press allowance built into the bore, set checked on one mandrel.

Flange Faced With the Bore

The flange face is finished in the same clamping as the bore, so it sits flat on the housing within 0.02 mm and the bushing does not cock when it is pressed home.

Bore Sized for the Press Fit

The bore is finished 0.01 mm over nominal to allow for the closure that happens during pressing, so the shaft clearance is right after installation rather than on the bench.

Oil Groove Cut Before Finishing

The groove is cut before the bore is finished, which removes the burr it raises; cutting it afterwards leaves a lip that scrapes the shaft on assembly.

Set Checked on One Mandrel

Every bushing in the set is slid onto the same mandrel and checked for rock; a set that is individually in tolerance can still bind if the bores sit at opposite ends of H7.

Bushing that must not close on pressing?

Finishes for Flanged Bushings

The bore is a running fit, the outside is a press fit, the flange is a seat.

FinishMain PurposeFinishMain Purpose
PassivationRemoves free iron after turningElectropolishingRa 0.4 µm bore for a sliding shaft
Bead BlastingEven matte on the flange faceMasked BoreBore stays H7
Oil GrooveRetains lubricant in a dry running bushLaser MarkingBore size and set number
Tin PlatingNon-stainless bronze variant onlyBore PlugKeeps grit out in transit
Press Fit CheckOutside diameter gauged to m6Set Trial FitAll bushings checked on one mandrel
Salt Spray500 h on 304Bore RecheckH7 After Passivation

*Electropolishing opens the bore 5 to 8 µm and is done before the final bore gauge check; a polished bushing is never reamed afterwards or the finish is lost.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
They pressed in square and the flange seated flat on the housing face.

Industrial Components Buyer
The shaft went through after pressing, which is what the bore allowance was for.

Equipment Manufacturer
All the bushings in the set took the same mandrel, so any of them fits any position.

OEM Customer
OEM Customer
No wear step in the bore after a year of oscillating load.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.

Trusted for Precision CNC Milling.

Turning a Flanged Bushing

The flange and the bore are finished in one clamping, so the bushing presses in square and the flange seats flat on the housing face.

01. Housing and Shaft Review

Confirm the housing bore, the shaft size and the axial load, then set the outside diameter and the bore allowance for the press.

02. Turn the Outside

Turn the outside to m6, face the flange square and part off with enough stock to face the second side.

03. Bore and Groove

Bore to H7, cut the oil groove if specified, then finish the bore with a sharp positive tool at low feed and check roundness in two planes.

04. Face the Flange

Face the flange to thickness at ±0.03 mm, square to the bore within 0.02 mm, and break both bore edges 0.3 mm.

05. Check, Passivate, Pack

Air gauge every bore, check the set on one mandrel, passivate, plug the bore and bag by set.

Send the housing bore and shaft diameter, and we will quote bushings with the bore sized for the press fit and the set checked on one mandrel.

Flanged Bushing FAQs

About 0.01 mm on a 2.5 mm wall into an m6 housing, and up to 0.02 mm on a thin wall. The bore is finished oversize by that amount so the shaft clearance is correct after pressing.

m6 into an H7 housing for a steel housing, p6 for aluminium. A tighter fit splits a thin housing, and a looser one lets the bushing turn in service.

In bronze, yes at low speed. In 304 stainless it will pick up on a stainless shaft, so either an oil groove or a bronze bush is specified for dry running.

Because a replacement bushing at the other end of H7 can bind on the same shaft. Matching the set within 0.05 mm means one shaft slides through all of them.

No, it only removes free iron. Electropolishing does, by 5 to 8 µm, so the bore is measured after polishing and before packing.

Yes, each piece can have its own flange, but the set is then matched on the bore only, and the pieces are marked so they go in the right position.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

CNC turned alloy steel threaded flange bases with an internal thread concentric to the spigot, flange face square to 0.02 mm, and.

CNC machined aluminium robot mounting brackets supplied as matched pairs, right-angle held to 0.05 mm, gusseted for stiffness and.

CNC machined aluminium circular positioning bases with a turned register, bolt circle to ±0.02 mm and a flat seating face, red or.

Precision CNC machined aluminum robot joint housings for arm segments and joint modules.

Precision CNC machined aluminum robot joint housing flanges.

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top