

Home / CNC-Machining / CNC Milling / CNC Machined Aluminum Robot Joint Housing
CNC Machined Aluminum Robot Joint Housing - CNC machined component

CNC Machined Aluminum Robot Joint Housing

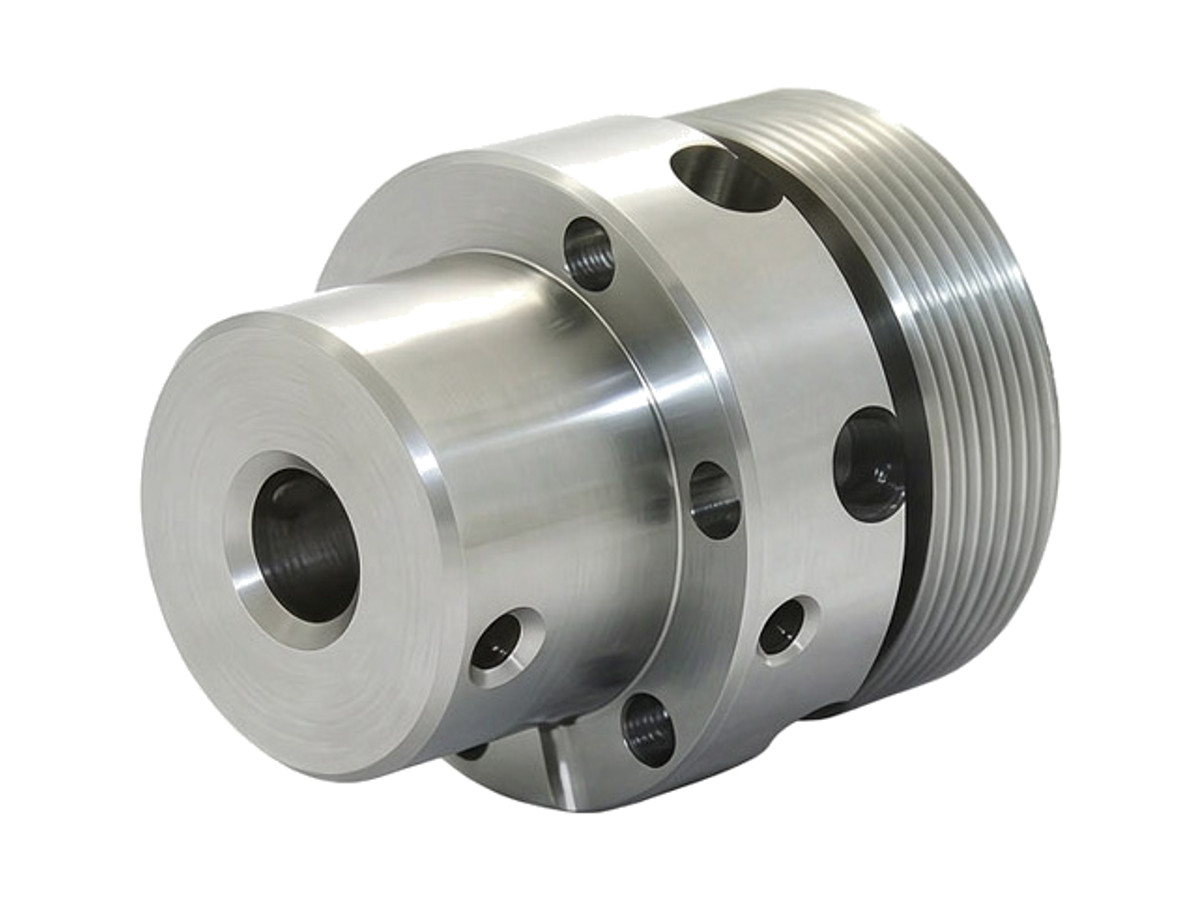
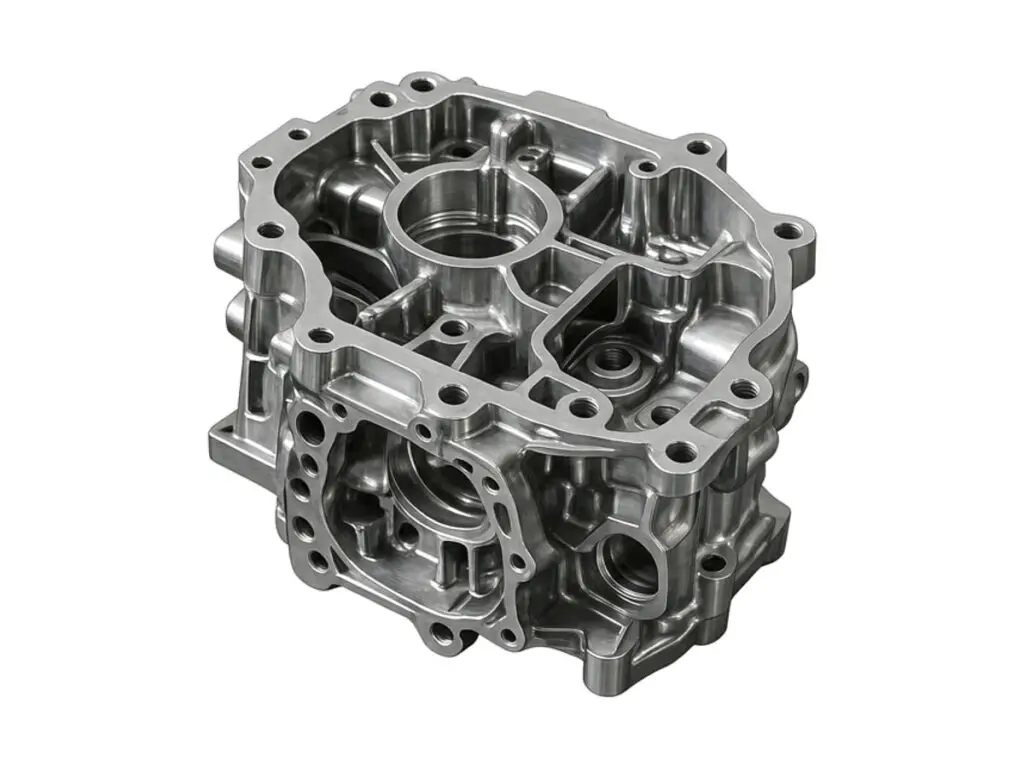
Custom CNC machined aluminum robot joint housings for arm segments and joint modules. Run on five axes with the bearing bores and seal grooves cut from one datum, so the joint turns on a single axis and the arm carries payload instead of its own structure.

*Send the joint torque and the cable route, because the rib layout and the cable path decide how much wall can be removed without losing stiffness.

Aluminum Robot Joint Housing Overview

A robot joint housing is the structure between two arm segments. It carries the joint torque, holds the bearing on one axis and routes the cable without chafing it, all while being as light as the payload allows.

The body is milled from a billet on five axes, with the outside profile and the inside core cut so the wall is even. Bearing bores and seal grooves are cut from one datum, which keeps the joint on a single axis and stops the arm from tracking a curve when it rotates.

Five-axis milling of an aluminum wrist housing for a robot arm
6061-T6 aluminium round bar stock for CNC turning

6061-T6 Aluminum Bar

6061-T6 round bar is the starting point for housings and discs that are turned before they are milled. The bar is centred once, so the bore, the outer diameter and the flange face share one axis, and the milling that follows is referenced to that axis rather than to an edge.

7075-T6 aluminium round disc blank for CNC machining

7075-T6 Aluminum Disc

7075-T6 disc stock is chosen when the part is thin, runs fast or carries a bearing. The higher strength lets a 6 mm web hold a bore without a boss, and the machined surface takes a hard anodized layer without the orange-peel that softer alloys show.

Weight and stiffness trade directly. A 3 mm wall with ribs carries the same torque as a 6 mm solid wall at half the mass, but only if the ribs run along the load path rather than across it.

Aluminum Robot Joint Housing Specifications

Machining data for joint housings, agreed against the joint torque, the cable route and the bearing stack.

SpecificationMachining DataSpecificationMachining Data
ProductRobot Joint Housing / Arm Segment BodyMachining Process5-Axis CNC Milling, CNC Boring
Material6061-T6 / 7075-T6 AluminumTypical Tolerance±0.02 mm on Bore, ±0.05 mm on Flange
Housing Size80 × 80 mm to 400 × 300 mmConcentricity0.01 mm Across Bearing Bores
Wall Thickness3 – 10 mmPerpendicularity0.02 mm Flange to Bore
Bearing Bore20 – 180 mm, H7Surface FinishRa 1.6 µm, Ra 0.8 on Bores
FeaturesRibbed Walls, Seal Grooves, Cable Path, Motor MountDrawing FormatSTEP, STP, IGES, X_T, DWG, DXF, PDF
CustomizationCable Route, Motor Interface, Rib Layout, ColourLead Time10 – 16 Days (Prototype), 20 – 30 Days (Batch)
InspectionCMM Coaxiality, Bore Gauge, Wall ScanPackingFoam Cradled, Bore Capped, Carton
Weight Range0.8 – 12 kg FinishedAnodizingType II 15 – 20 µm

Key Features of Our CNC Machined Joint Housings

Light where the load allows, rigid where the joint turns.

Five-Axis Profile Machining

The outer profile and the internal core are cut on five axes in one set-up, so the wall stays even around the joint and the weight comes off where it does not carry load.

Bearing Bores on One Axis

Both bores are cut from the same datum, so the joint turns on a single axis and the arm does not track a curve as it rotates.

Cable Path Machined In

The cable route is machined into the body with radiused entries, so the harness does not chafe as the joint moves through its range.

Seal Grooves Cut to Drawing

Seal grooves are cut last, from the finished face, so the compression is what the drawing specifies rather than what the rough stock allowed.

Arm that drifts or chafes its cable?

Surface Finishes for CNC Machined Joint Housings

The finish on a joint housing is both cosmetic and functional, so bores and grooves are protected separately.

FinishMain PurposeFinishMain Purpose
As MachinedBare body where it sits under an arm coverType II AnodizingCorrosion protection and colour on the arm
Hard AnodizingWear resistance on the seal and bearing landsBead BlastingMatte face before dyeing
Masked BoresBearing bores left bare to hold the H7 fitLaser MarkingJoint number and axis direction

*Anodizing adds 15 to 20 µm and closes a bore. Bearing bores and seal grooves are masked before the bath, or cut oversize by the coating thickness where masking is impractical.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
The arm tracks straight through the joint range now, which it did not with the previous housing.

Industrial Components Buyer
Weight came down without losing stiffness, and our payload rating went up as a result.

Equipment Manufacturer
The cable path has radiused entries, so the harness has not chafed since we installed it.

OEM Customer
OEM Customer
Seal grooves were right, so the joint is dry after six months of continuous cycling.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.

Trusted for Precision CNC Milling.

CNC Machining Process for Aluminum Joint Housings

The body is machined from a billet and cored from the inside, so the arm loses weight where it does not carry load.

01. Torque and Route Review

Check the joint torque, the bearing stack and the cable route against the wall thickness, and adjust the rib layout where the torque is highest.

02. Billet and Roughing

Select billet with stock on all faces, rough the outer profile and the internal core, then let the part relax before the finishing passes.

03. Five-Axis Finishing

Finish the outer profile, the bores and the cable path in one set-up, keeping the tool normal to the surface so the wall thickness stays even around the joint.

04. Grooves and Coating

Cut the seal grooves from the finished face, break the cable path edges, then mask the bores and anodize to the agreed colour.

05. Inspection and Packing

Check coaxiality, flange squareness and wall thickness on a CMM, cap the bores, and pack with foam so the anodized faces are not marked.

Have a joint that drifts under load or a cable that wears through? Send the joint drawing and the cable route, and we will quote the housing that fixes it.

CNC Machined Aluminum Robot Joint Housing FAQs

A ribbed 3 mm wall typically saves 35 to 45 percent against a 6 mm solid wall while holding the same torque, provided the ribs follow the load path between the bearing bosses.

The outer profile, the internal core and the cable path are not reachable in one three-axis set-up. Five-axis machining cuts them without re-clamping, which keeps the wall even and the bores on one axis.

Yes. The route is cut with radiused entries and a smooth floor, so the harness does not chafe as the joint sweeps through its range.

Bearing bores and seal grooves are masked before the bath, or cut oversize by the coating thickness where masking is not practical, so the H7 fit survives.

Yes, when both halves are quoted together. Machining both from one datum is what keeps the joint axis aligned across the arm.

Ten to sixteen days for a single housing including five-axis programming, machining, coating and inspection. Batches of 20 or more run twenty to thirty days.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

Custom CNC machined aluminium fuel pump blocks for automotive and motorsport fuel systems.

Custom CNC machined hardened steel sleeves for robotic joints and motion assemblies.

Custom CNC machined aluminum double tube clamps for motorcycle frames, bicycle builds and hydraulic lines.

CNC Machined Stainless Steel Rotary Joint Housing

CNC Machined Stainless Steel Automation Fixture

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top