Home / CNC-Machining / CNC-Turning / CNC Turned Aluminum Threaded Hose Fitting
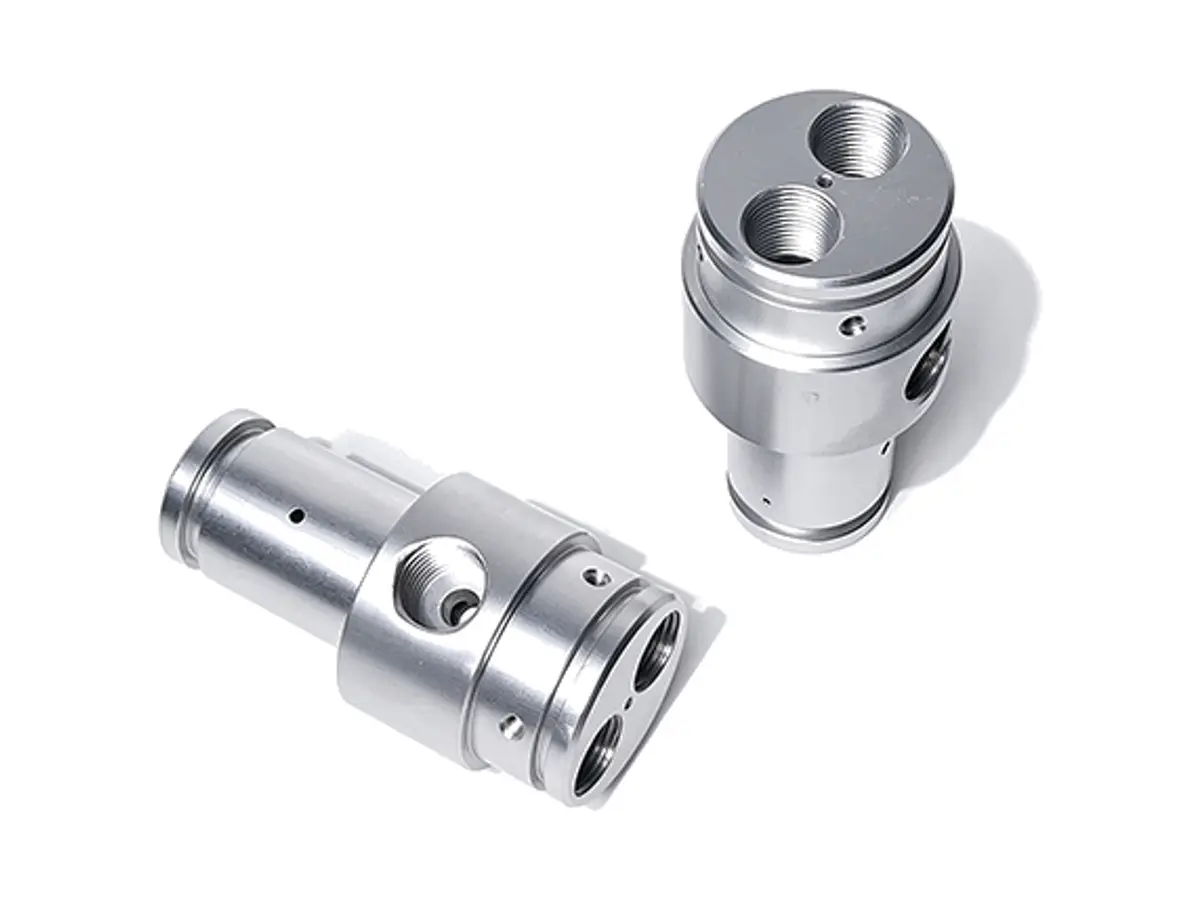
CNC turned anodized aluminium threaded hose fittings with a barbed spigot and a sealing face

CNC Turned Aluminum Threaded Hose Fitting

6061-T6 aluminium hose fittings turned with a threaded or barbed spigot, a sealing face square to the thread within 0.03 mm and the spigot coaxial to the thread within 0.05 mm. Anodized in colour with the threads and barbs masked, so the fitting still assembles by hand after coating.

*Tell us the hose type and the working pressure. A barb for a braided hose is not the same as one for a push-on liner, and the wrong barb either leaks or cuts the tube.

Threaded Hose Fitting Overview

A fitting has to do two things at once: seal against a port and grip a hose. The seal depends on the face being square to the thread, and the grip depends on the barb being formed to the hose liner rather than cut into it.

The fitting is turned from bar in one cycle, with the thread cut last so the sealing face can be used as the reference. Barbs are formed with a profile tool that rolls the material rather than a sharp insert that leaves a cutting edge, then the bore is deburred from both ends.

Assembly and inspection of a rod end clevis, a slotted drive hub and a split clamp ring
6061-T6 aluminium round bar stock for CNC turning

6061-T6 Aluminium Bar

6061-T6 is used for pneumatic and low-pressure hydraulic fittings where weight matters, and it anodizes to a colour that identifies the circuit at a glance on a crowded manifold.

7075-T6 aluminium round disc blank for CNC machining

7075-T6 or 316 Stainless

7075 is chosen where the thread sees repeated assembly and the aluminium would wear. Stainless is specified above about 20 bar or in any wet environment, where an anodized thread would corrode into the port.

Pressure and reassembly count decide the material, not the hose size. An aluminium fitting that is taken off twice a year will gall its thread long before a stainless one does.

Threaded Hose Fitting Specifications

Turning data for hose fittings, with the thread, seal face and barb values that decide whether the joint seals and the hose stays on.

SpecificationMachining DataSpecificationMachining Data
ProductThreaded Hose Fitting / AdapterMachining ProcessCNC Turning, Threading, Forming, Deburring
Material6061-T6 Aluminium BarThread SizeM8 – M30, BSP, NPT, UNF
Hose Spigot6 – 25 mm Barb or ThreadCoaxialityThread to Spigot 0.05 mm
Sealing FaceSquare to Thread 0.03 mmHex Flats14 – 36 mm Across Flats
BoreØ 4 – 20 mm ThroughSurface FinishRa 1.6 µm Seal Face, Ra 3.2 µm Body
AnodizingType II 15 – 25 µm, Threads and Barbs MaskedPressure RatingUp to 20 bar Pneumatic, 10 bar Hydraulic Return
CustomizationSwivel Nut, Elbow, Bulkhead, O-Ring GrooveLead Time4 – 6 Days Sample, 10 – 13 Days Batch
InspectionThread Plug Gauge, Seal Face Squareness, Bore Gauge, Leak TestPackingThread Caps, Bagged, Carton

Key Features of Our Hose Fittings

Seal face square, barb formed, threads masked.

Seal Face Square to the Thread

The face is turned from the same axis as the thread and held to 0.03 mm, so a bonded washer or an O-ring seals on the first tightening instead of needing a second nip.

Barbs Formed, Not Cut

The barb profile is rolled with a form tool, which leaves a radius on the crest instead of a knife edge, so the hose liner is gripped without being cut.

Spigot Coaxial to the Thread

Both features are cut in one cycle, holding coaxiality to 0.05 mm, so the hose does not sit at an angle and load the fitting sideways.

Threads and Barbs Masked

Plugs and caps protect the functional surfaces during anodizing, and every thread is gauged after coating before the fitting is packed.

Fitting that has to seal and hold the hose?

Surface Finishes for Hose Fittings

Colour identifies the circuit; the thread and the barb have to stay functional underneath it.

FinishMain PurposeFinishMain Purpose
Type II AnodizingColour coding by circuit and corrosion protectionMasked Threads and BarbsKeeps threads at gauge and barbs at grip size
Hard AnodizingWear resistance where hoses are pushed on and offBead BlastingMatte body before dye
Laser MarkingThread size and circuit code on the hexPTFE Tape Pre-AppliedSealing without a separate tape at assembly

*Anodizing adds 7 to 12 µm per surface, which is enough to stop a thread starting by hand. Threads are masked and gauged, and barbs are capped so the grip diameter is unchanged.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
Sealed at the first nip, with no tape needed on the face seal.

Industrial Components Buyer
The barb held the hose at 12 bar without a ferrule, and it has not crept.

Equipment Manufacturer
Threads start by hand, and the anodizing did not change the fit.

OEM Customer
OEM Customer
Colour coding by circuit means our fitters pick the right one first time.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.

Trusted for Precision CNC Milling.

Turning Process for Hose Fittings

The spigot is formed rather than cut, so the barb grips the hose liner without a sharp edge that would slice it under pressure.

01. Hose and Port Review

Confirm the hose type, the barb style, the port thread and the working pressure, and check the bore against the flow the circuit needs.

02. Turn the Body

Face the bar, turn the hex and the body, and turn the sealing face first so it can be used as the reference for the thread.

03. Thread and Form the Spigot

Cut the thread to a pre-plate size and form the barb with a profile tool, keeping both on the same axis so the hose runs straight.

04. Bore and Deburr

Drill and bore through, then deburr both ends and the barb roots, since a burr inside the bore restricts flow and a burr on a barb cuts the liner.

05. Mask, Anodize and Gauge

Cap the barbs, plug the threads, anodize to colour, then gauge every thread and check the seal face before fitting protective caps.

Send the hose specification and the port thread, and we will quote the fitting with the barb matched to the hose you run.

Threaded Hose Fitting FAQs

A double-barb profile with a longer lead-in, because the braid needs to be pushed past two crests before the ferrule compresses. A single barb is for push-on liner hose at low pressure.

About 20 bar pneumatic and 10 bar on a hydraulic return line. Above that, stainless or steel is the correct material regardless of weight.

It would, by about 20 µm on the diameter, so the thread is masked and cut to a pre-plate size. Every fitting is gauged after coating.

Yes, a face or radial O-ring groove can be turned in the same cycle, with the groove depth and width to the O-ring drawing.

0.03 mm to the thread axis, checked with a dial indicator on a threaded mandrel. That is what allows a bonded washer to seal at the first torque.

Yes, a sample from each batch is assembled to a test port and held at 1.5 times the rated pressure. Every fitting is gauged, but the leak test is by sample unless you ask for 100 %.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

Custom Brake Lever CNC Milled components manufactured with precision CNC machining, supporting OEM customization, lightweight.

CNC machined aluminium robot mounting brackets supplied as matched pairs, right-angle held to 0.05 mm, gusseted for stiffness and.

316L stainless multi-port valve bodies machined from solid, port faces flat to 0.02 mm and cross-drilled galleries pressure.

Custom five-axis CNC milled 316L stainless steel mixing impellers for agitators and reactors.

Precision CNC machined stainless steel control valve bodies with lapped sealing faces and gauged ports.

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top