

Home / CNC-Machining / CNC Milling / CNC Machined Stainless Serrated Blade and Jaw Set
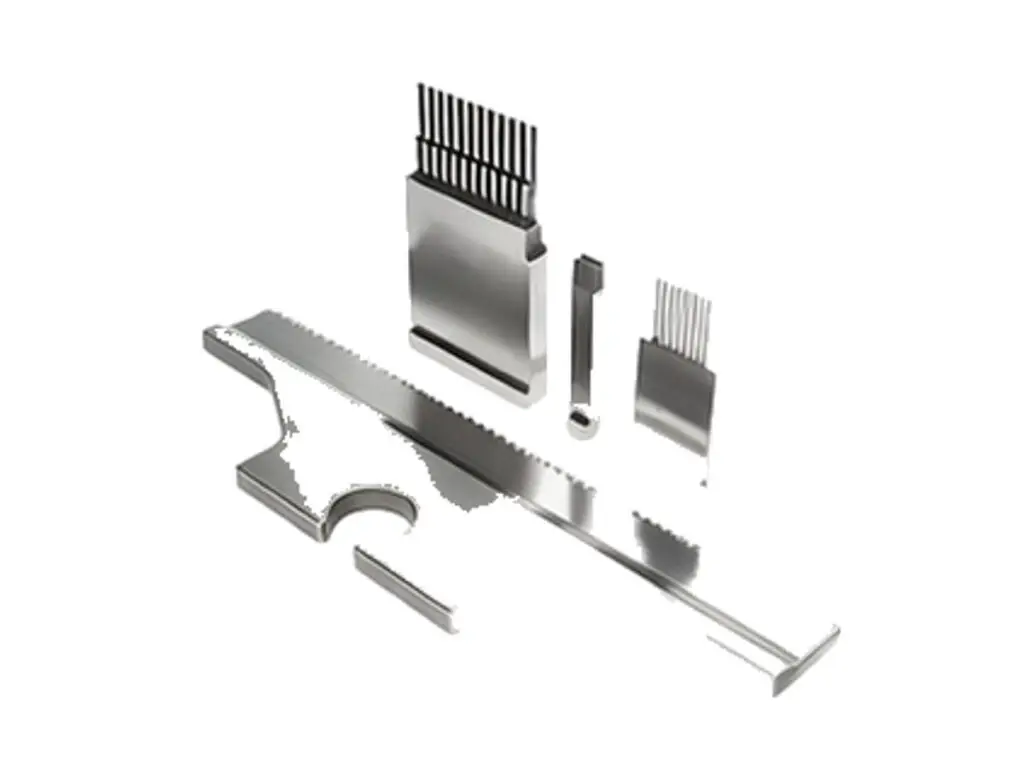
CNC machined 304 stainless serrated blade and matching comb jaw set

CNC Machined Stainless Serrated Blade and Jaw Set

Serrated blades and comb jaws machined from 304 stainless: a 180 mm blade with a 0.8 mm tooth pitch held to ±0.02 mm, 1.2 mm tooth height, 0.05 mm edge radius and straightness of 0.03 mm over the full length. The matching comb jaw carries twelve 0.9 mm slots on a 1.6 mm pitch so the blade passes through without contact.

*Send a sample of the material being cut. Tooth pitch and edge radius are set from the web thickness, and a blade that is 0.02 mm too thick will bind in the comb instead of shearing.

Stainless Blade and Comb Jaw Overview

A serrated blade only works if the teeth are uniform, the edge is sharp without being fragile, and the blade stays straight along its whole length. The comb jaw then has to hold the slots at exactly the blade pitch, or the blade rubs and the cut edge frays.

The blank is milled to thickness, the teeth are roughed with a 0.8 mm end mill and finished by wire EDM so the roots are square, and the edge is honed to a 0.05 mm radius. The comb slots are cut in one pass on the wire with the same pitch reference, and both parts are passivated together.

Assembly and inspection of a rod end clevis, a slotted drive hub and a split clamp ring
304L stainless steel round bar stock for CNC machining

304 Stainless Steel

304 gives a blade that resists staining in a wet process line and holds a fine tooth at 42 HRC after stress relief, without the brittleness of a 440C edge.

304L stainless steel plate and block stock for CNC machining

316L or 420

316L is used for food and medical lines where chloride attack is a risk, and 420 is chosen when the blade runs against an abrasive web and needs higher hardness.

A blade thinner than 1.2 mm will bow when the teeth are milled; the thickness is set at 1.5 mm and relieved only behind the tooth line.

Serrated Blade Specifications

Tooth, slot and edge data, expressed the way a blade is actually measured.

SpecificationMachining DataSpecificationMachining Data
ProductSerrated Blade and Comb Jaw SetProcessCNC Milling, Wire EDM, Grinding
Material304 Stainless SteelBlade Length180 mm ±0.10 mm
Tooth Pitch0.8 mm ±0.02 mmTooth Height1.2 mm ±0.03 mm
Blade Thickness1.5 mm ±0.02 mmStraightness0.03 mm Over 180 mm
Comb Jaw Slots0.9 mm Wide, 12 SlotsSlot Pitch1.6 mm ±0.02 mm
Cutting EdgeRadius 0.05 mm, No BurrHardnessHRC 42 After Stress Relief
Mounting Holes2 × Ø4 H7, ±0.03 mmWeightApprox. 62 g per Set
InspectionProfile Projector, Edge MicroscopeBatch Size50 to 5,000 Sets
FinishPassivation, No Coating on EdgeDrawing FormatDXF, STEP, PDF

Teeth That Cut, Not Tear

Wire-cut roots, a honed edge and a comb cut to the same pitch.

Teeth Wire-Cut, Not Milled Through

The tooth roots are finished on the wire so they are square and identical, which stops one tooth from standing proud and taking the whole cut load.

Edge Honed to a Controlled Radius

A 0.05 mm radius is put on the cutting edge under a microscope, sharp enough to shear the web and strong enough that the tip does not chip on the first stroke.

Blade and Comb Cut to One Pitch

The comb slots and the blade teeth are cut from the same pitch reference, so the blade passes through the comb with 0.05 mm clearance per side instead of rubbing.

Straightness Checked on a Granite

Each blade is checked for straightness over its full 180 mm on a granite plate, and any blade over 0.03 mm is straightened before passivation.

Blade set that has to shear cleanly?

Surface Finishes for Blade Sets

The body can be coated, the edge cannot; masking decides which is which.

FinishMain PurposeFinishMain Purpose
PassivationRemoves free iron after machiningElectropolishingBurr-free cutting edge
Bead BlastingMatte body, masked teethLaser MarkingBatch and tooth count
Black OxideLow-reflection bodyTitanium NitrideWear life on abrasive stock
Masked EdgeEdge kept bare and sharpUltrasonic CleanRemoves polishing compound
Deburr OnlyBlade used in a wet processEdge HoningControlled 0.05 mm radius
Oil DipShort-term rust protectionVCI WrapBlades shipped sharp and dry

*Electropolishing removes 3 to 5 µm from every surface, which dulls a 0.05 mm edge; the edge is masked when the body is polished.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
The teeth are uniform along the full length, so the cut edge stopped fraying.

Industrial Components Buyer
The blade passes through the comb without rubbing, exactly as the clearance was quoted.

Equipment Manufacturer
The edge is still sharp after a full shift, which our previous supplier could not manage.

OEM Customer
OEM Customer
The set arrived matched, so we did not have to pair blades and combs ourselves.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.

Trusted for Precision CNC Milling.

How We Machine a Blade and Comb Set

The teeth are milled at a 0.8 mm pitch and then wire-cut to a 0.05 mm edge radius, so the blade cuts instead of tearing the web.

01. Web and Machine Review

Check the web thickness, the cut length and the machine stroke, then set the tooth pitch and the edge radius from the material sample.

02. Mill the Blank

Mill the blank to 1.5 mm with a 0.3 mm finish allowance on both faces, drill the mounting holes and stress-relieve before the teeth are cut.

03. Rough and Wire the Teeth

Rough the tooth gaps with a 0.8 mm end mill, then wire-cut every root to the final profile so the pitch stays within 0.02 mm over the full length.

04. Cut the Comb Slots

Set the comb on the same pitch reference and wire-cut twelve 0.9 mm slots, checking the pitch with a pin gauge before removing the part.

05. Hone, Passivate, Inspect

Hone the cutting edge to a 0.05 mm radius under a microscope, passivate both parts and inspect the tooth profile on a projector.

Send a sample of the material being cut and the blade drawing, and we will quote a matched blade and comb with the pitch set to your web.

Serrated Blade and Jaw FAQs

From 0.5 mm to 4 mm. Below 0.8 mm the tooth is wire-cut only, since an end mill that small cannot clear the chips at a production rate.

A 0.05 mm radius, checked under a 20× microscope. A true knife edge is not used because it rolls over on the first stroke in stainless.

TiN and DLC are both possible on the body, but the cutting edge is masked so the coating does not blunt it.

Yes, and it is the recommended way to buy the set. Both parts are cut from the same pitch reference so the clearance is known rather than measured afterwards.

The blade is stood on a granite plate against a dial indicator over its full length, and any deviation over 0.03 mm is corrected before passivation.

Fifty sets for a new profile, since the wire program and the edge honing fixture are made for the part.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

CNC machined 6061-T6 aluminium lightening hole cover plates with a 38 % open face, a 25 mm solid fixing frame, holes within 0.08.

CNC turned 6061-T6 aluminium V-belt pulleys with a ground bore, machined V-groove to 0.05 mm, balanced rim and keyway, anodized.

CNC machined 316L stainless steel pump connector plates with a lapped seal face, a bored port and a bolt pattern within 0.03 mm,.

CNC machined 6061-T6 aluminium control levers with a machined pivot bore, a tapered grip section and a cable slot, held to a.

CNC turned 6061-T6 aluminium rod end joint fittings with a threaded stem, a cross-drilled eye and a flat-faced fork, anodized in.

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top