


Home / CNC-Machining / CNC Milling / CNC Machined Aluminum Gearbox Housing
CNC Machined Aluminum Gearbox Housing - CNC machined component

CNC Machined Aluminum Gearbox Housing

Custom CNC machined aluminum gearbox housings for robot joints, conveyors and test rigs. Split halves are machined, bolted and line bored together, so the bearing seats are coaxial to 0.01 mm across the housing and the shafts do not preload the bearings.

*Send the shaft centres and the gear drawing, because the seat positions, the split face height and the oil level all follow from the gear mesh rather than from the outline.

Aluminum Gearbox Housing Overview

A gearbox housing holds two or more shafts at fixed centres, and it holds them while the gears push the shafts apart. If the bearing seats are not coaxial across the split, the bearings run preloaded and the gearbox whines before it fails.

The two halves are machined, bolted together and then line bored as one body, so the seats share an axis regardless of how the split face cleaned up. The split face is finished flat to 0.02 mm so the halves close without a gasket step, and the oil gallery and breather are cut before the final bore.

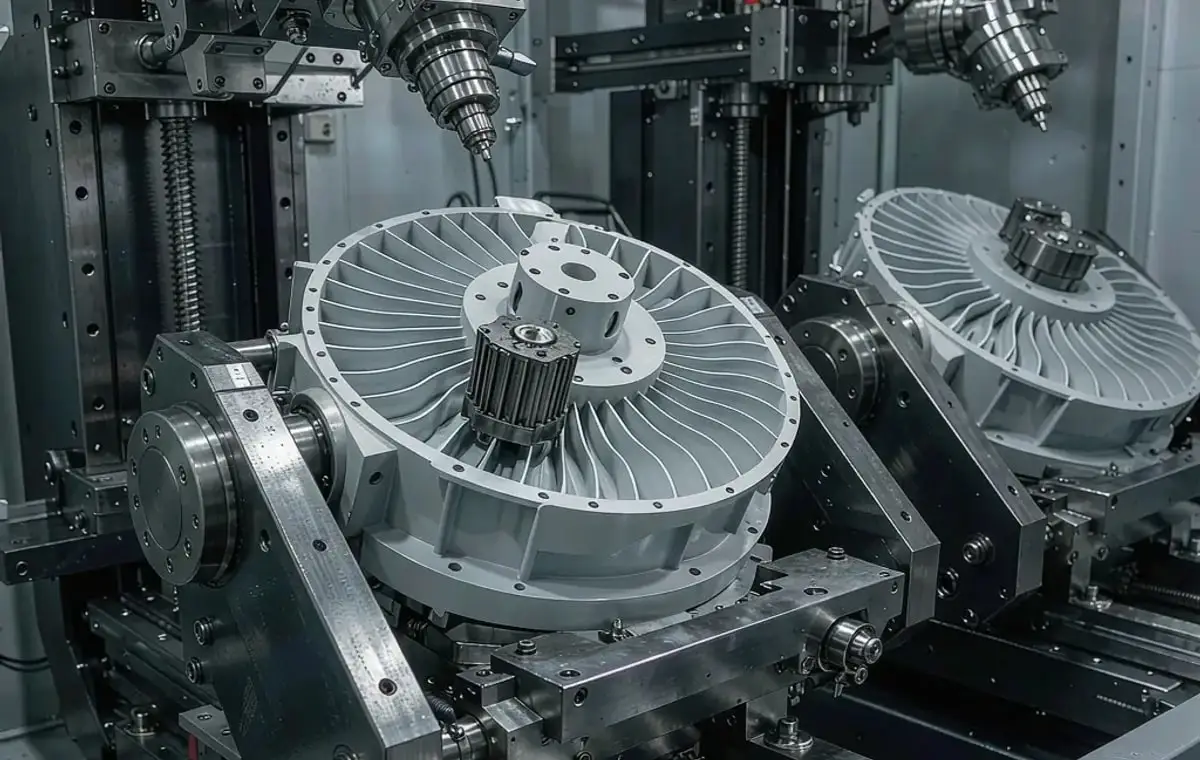
Five-axis machining of a vacuum pump impeller and a twin-body valve housing
6061-T6 aluminium flat plate stock for CNC milling

6061-T6 Aluminum Plate

6061-T6 is the default for brackets and plates that are anodized after machining. It cuts cleanly at high spindle speed, keeps a flat face through thin sections, and takes a uniform dye colour without blotching, which matters when two parts have to match visually.

7075-T6 aluminium billet block stock for CNC milling

7075-T6 Aluminum Billet

7075-T6 is used where the part carries load or runs at high cycle rate. Its yield strength is close to mild steel at a third of the weight, so a bracket can be thinner and still hold stiffness. It anodizes to a deeper colour and machines with a better surface, at a higher billet cost.

Housing stiffness matters more than alloy strength. A ribbed 6061 housing usually outperforms a solid 7075 one because the ribs carry the gear separation load without adding mass at the seats.

Aluminum Gearbox Housing Specifications

Machining data for split gearbox housings, agreed against the shaft centres and the gear separation load.

SpecificationMachining DataSpecificationMachining Data
ProductGearbox Housing / Split Gear CaseMachining ProcessCNC Turning, 4-Axis Milling, Line Boring
Material6061-T6 / 7075-T6 AluminumTypical Tolerance±0.02 mm on Bearing Seats, ±0.05 mm on Outline
Housing Size100 × 100 mm to 500 × 400 mmSeat Coaxiality0.01 mm Across the Housing
Bearing Seat Diameter20 – 160 mm, H7Split Face Flatness0.02 mm
Wall Thickness4 – 15 mmSurface FinishRa 1.6 µm, Ra 0.8 on Seats
FeaturesSplit Face, Bearing Seats, Breather, Drain, Oil GalleryDrawing FormatSTEP, STP, IGES, X_T, DWG, DXF, PDF
CustomizationShaft Centres, Split Position, Port Layout, ColourLead Time10 – 16 Days (Prototype), 22 – 32 Days (Batch)
InspectionCMM Coaxiality, Split Face Flatness, Leak TestPackingSplit Faces Protected, Crate
Weight Range1 – 25 kg FinishedAnodizingType II 15 – 20 µm

Key Features of Our CNC Machined Gearbox Housings

Seats that share an axis after the halves are bolted, not before.

Line Bored After Assembly

The halves are bolted together and bored as one body, so the seats are coaxial to 0.01 mm even if the split face cleaned up unevenly.

Split Face Flat to 0.02 mm

The split face is finished flat, which lets the halves close without a gasket step that would offset the seats.

Ribbed Load Path

Ribs run from the bearing bosses to the mounting feet, so the gear separation load goes into the frame instead of bending the housing wall.

Oil and Breather Provision

Oil galleries, drain and breather ports are machined before the final bore, so no chip enters a finished seat.

Gearbox whining after a rebuild?

Surface Finishes for CNC Machined Gearbox Housings

A gearbox housing is usually visible and always oil tight, so the finish and the seats are treated separately.

FinishMain PurposeFinishMain Purpose
As MachinedBare housing where it is hidden behind a guardType II AnodizingCorrosion protection and colour on visible cases
Bead BlastingMatte face before dyeing, hides tool marksSealed AnodizingCloses the coating on wet or washdown gearboxes
Masked SeatsBearing seats left bare to hold the H7 fitLaser MarkingShaft centres and oil level marks

*Anodizing is porous unless sealed. A gearbox that sees washdown uses sealed anodizing, and the bearing seats are masked so the H7 fit survives the bath.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
The gearbox runs quiet after assembly, and the seats were coaxial across the split without any shimming.

Industrial Components Buyer
Split face closed metal to metal with a thin sealant, so we did not need the gasket that used to offset the seats.

Equipment Manufacturer
Oil gallery and breather were already in the right place, so the lubrication circuit did not need rework.

OEM Customer
OEM Customer
They line bored after bolting the halves, which is the detail that made the difference for us.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.
Trusted for Precision CNC Milling.

CNC Machining Process for Aluminum Gearbox Housings

Both bearing seats are line bored through the assembled halves, so the shafts sit on one axis instead of two.

01. Shaft and Gear Review

Check the shaft centres, the gear widths and the separation load, then confirm the split position and the rib layout before machining.

02. Half Machining

Machine each half from billet with the split face as the datum, leaving stock on the bearing seats for the line boring operation.

03. Bolting and Line Boring

Bolt the halves together on a fixture and line bore both seats in one pass, which is what makes the seats coaxial across the split.

04. Ports and Coating

Drill the oil gallery, drain and breather, deburr internally, then mask the seats and anodize to the agreed colour.

05. Leak Test and Inspection

Assemble with a blanking plate, leak test the oil chamber, then check coaxiality and split face flatness on a CMM before packing.

Have a gearbox that runs hot or noisy after assembly? Send the shaft centres and gear drawing, and we will quote the housing that holds the axis.

CNC Machined Aluminum Gearbox Housing FAQs

Boring each half separately makes the seats depend on how the split face cleaned up. Bolting first and boring through guarantees the seats share an axis, which is what stops the bearings running preloaded.

Finished flat to 0.02 mm, which lets the halves close metal to metal with a thin sealant rather than a gasket that would offset the seats.

Yes, if you send the mating frame or a drawing. The housing is programmed from the measured interface so it bolts to the existing frame without re-drilling.

Four millimetres is the practical minimum for a housing up to about 250 mm, with ribs carrying the load. Thinner walls deflect under gear separation load and the seats move.

The housing is machined to the seat sizes you specify. Gears and bearings can be sourced and fitted as an assembly where the gearbox is supplied complete.

Ten to sixteen days for a single housing including half machining, line boring, coating and leak testing. Batches of 20 or more run twenty-two to thirty-two days.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

Custom CNC machined aluminium housings for automation and electronic equipment.

Custom CNC machined aluminium indexing disks for rotary positioning systems.

Custom CNC machined stainless steel multi jaw clamping plates for lathe, grinder and wheel hub fixtures.

CNC Machined Aluminum Intake Manifold

CNC Machined Robot Joint Housing Flange

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top