


Home / CNC-Machining / CNC Milling / CNC Machined Anodized Tattoo Machine Frame
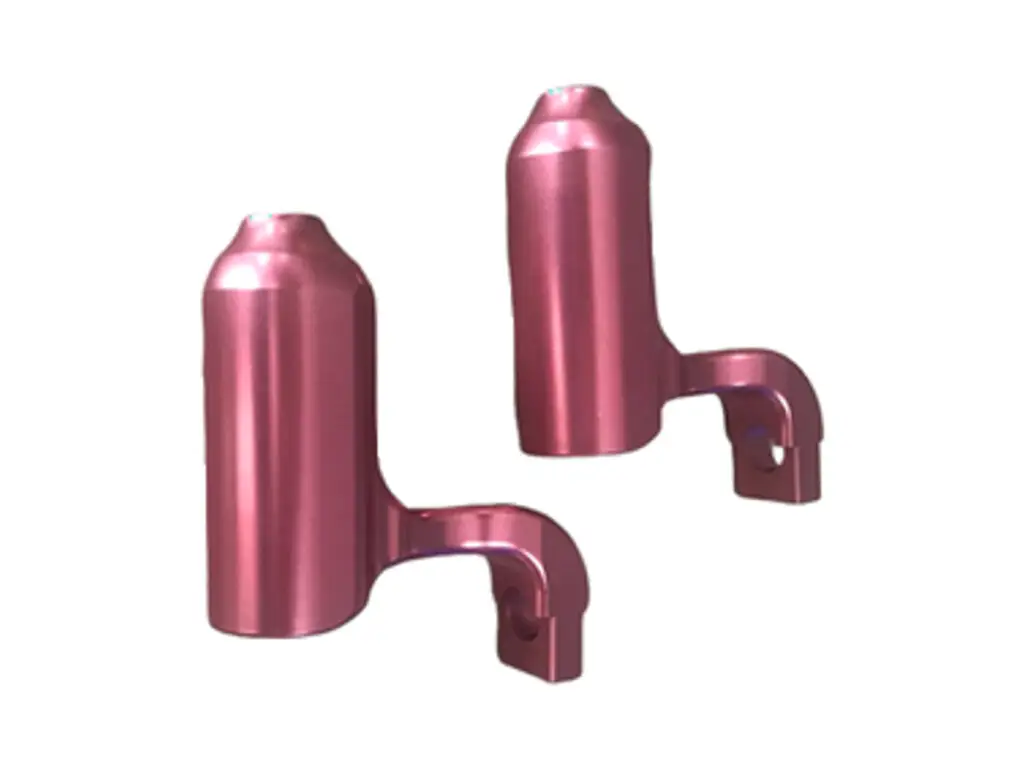
Pink anodized CNC machined aluminium tattoo machine frame with a Ø10 H7 armature bore

CNC Machined Anodized Tattoo Machine Frame

Tattoo machine frames machined from 6061-T6: 75 × 32 × 22 mm, a Ø10 H7 armature bore round within 0.008 mm, faces parallel to 0.02 mm, a 6 mm slot at ±0.03 mm and two M4 threads. Each frame is balanced to within 0.5 g and anodized in a sealed pink that resists hand oils and cleaning agents.

*Send the armature diameter and the grip thread. A bore 0.015 mm tight will bind the armature when the frame warms up in the hand, and the machine will run hot within a minute.

Anodized Machine Frame Overview

A hand-held machine frame has to hold an armature true, stay balanced in the hand and survive constant contact with skin, sweat and cleaning fluid. The bore and the grip faces are the two features that decide whether it runs smoothly, and both are cut from one set-up.

The frame is profiled from solid, the armature bore is bored and reamed to H7, and the grip faces are fly-cut so they stay parallel to the bore axis. The frame is weighed and balanced before anodizing, because coating adds about 0.6 g and that is enough to change the feel.

Assembly and inspection of a rod end clevis, a slotted drive hub and a split clamp ring
6061-T6 aluminium flat plate stock for CNC milling

6061-T6 Aluminium

6061-T6 gives a 42 g frame that dampens vibration better than a plastic shell and takes a sealed anodized finish that withstands alcohol wipes.

7075-T6 aluminium billet block stock for CNC milling

7075-T6 or Titanium

7075-T6 is used when the frame is machined thinner for a lighter feel, and Grade 5 titanium is chosen for premium frames where the anodized colour is produced by oxidation of the metal itself.

A wall under 3 mm at the grip will flex under hand pressure and change the armature clearance; the wall is kept at 4 mm.

Tattoo Machine Frame Specifications

Bore, balance and finish values for a frame that is held, not bolted.

SpecificationMachining DataSpecificationMachining Data
ProductTattoo Machine FrameProcessCNC Milling, Boring, Profiling
Material6061-T6 AluminiumEnvelope75 × 32 × 22 mm
Armature BoreØ10 H7, Roundness 0.008 mmBore Position±0.02 mm
Face Parallelism0.02 mmWall Thickness4 mm ±0.05 mm
Slot Width6 mm ±0.03 mmThreads2 × M4 × 0.7, 8 mm Deep
WeightApprox. 42 gEdge Break0.3 mm on Handling Edges
AnodizingPink, 18 to 22 µm, SealedBalanceMass Centred Within 0.5 g
InspectionBore Gauge, Balance CheckBatch Size25 to 2,000 Pieces
FinishAnodizing, Colour MatchedDrawing FormatSTEP, DXF, PDF

Bore, Balance, Feel

Bored and reamed in one clamping, balanced before coating.

Bore Bored and Reamed to H7

The armature bore is drilled, bored and reamed in a single clamping, giving 0.008 mm roundness so the armature turns without a tight spot at one point of its rotation.

Grip Faces Fly-Cut Parallel

Both grip faces are fly-cut after profiling and stay parallel to the bore axis within 0.02 mm, so the frame does not rock in the hand and the grip sits square.

Balanced Before Anodizing

Each frame is weighed and material is relieved from the rear boss until the mass centre is within 0.5 g, which is the difference between a frame that feels neutral and one that pulls.

Sealed Anodizing

The pink coating is sealed in a hot bath after dyeing, so it resists alcohol and disinfectant instead of fading at the grip within a few weeks of use.

Frame that has to run smooth in the hand?

Surface Finishes for Machine Frames

Colour and sealing matter as much as the coating thickness here.

FinishMain PurposeFinishMain Purpose
Pink AnodizingProduct identity, sealed surfaceBlack AnodizingLow-reflection frames
Clear AnodizingNeutral machined lookHard AnodizingWear face at the grip
Bead BlastingMatte before colourLaser MarkingSerial under the grip
Masked BoreBare bore for the armatureChromate ConversionConductive frame for grounding
Colour MatchFrame and grip in one shadeUltrasonic CleanCompound removal before sealing
Deburr OnlyFrames that will be polishedFoam PackingNo contact marks in transit

*An unsealed dye will fade where the hand contacts the frame; every frame is sealed, and the bore is masked so the armature fit is unchanged.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
The armature runs without a tight spot through the full rotation.

Industrial Components Buyer
The frame balances in the hand, which our testers noticed straight away.

Equipment Manufacturer
The bore stayed at size after anodizing, so no reaming was needed.

OEM Customer
OEM Customer
The pink finish has held up to daily cleaning with alcohol wipes.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.

Trusted for Precision CNC Milling.

How We Machine a Machine Frame

The armature bore and the grip faces are cut in one clamping, so the armature runs true and the frame does not buzz against the grip.

01. Armature and Grip Review

Check the armature diameter, the grip thread and the spring travel, then set the bore tolerance and the slot position from the drawing.

02. Profile the Frame

Profile the outer shape from solid with a 10 mm end mill, leaving 0.3 mm on the grip faces and the bore boss for finishing.

03. Bore and Ream

Drill the armature bore undersize, bore it to 0.05 mm under H7 and ream to size, checking roundness and bore position against the datum.

04. Fly-Cut Faces and Balance

Fly-cut both grip faces parallel to the bore, cut the 6 mm slot, tap the M4 threads and relieve the rear boss until the frame balances.

05. Anodize, Seal, Check

Deburr all edges, pink anodize, seal in a hot bath, then re-check the bore and the balance after coating.

Send the armature diameter and the grip drawing, and we will quote a frame with the bore reamed to H7 and the balance set before anodizing.

Tattoo Machine Frame FAQs

Yes, from a sample or a drawing. The armature bore, the grip thread and the slot position are the three features that have to match, and we copy them from the part.

It is weighed on a balance stand and material is removed from the rear boss in small steps until the mass centre sits within 0.5 g of the grip axis.

The bore is masked, so the H7 fit stays. If the bore is coated for wear, it is reamed back to H7 after anodizing.

The full anodizing range, including pink, black, clear, blue and gold. Custom dye lots are possible above 200 frames.

Yes, in Grade 5, with the colour produced by anodizing the titanium itself. The lead time is longer and the cost is roughly three times the aluminium frame.

H7 on the bore with the armature ground to h6 gives a light running fit. The clearance is agreed from the armature drawing before machining.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

CNC machined aluminium perforated mounting plates with a lightening hole pattern, edge datum faces and counterbored fixings, flat.

CNC machined 6061-T6 aluminium mounting brackets with a machined mounting face, slotted holes and an even anodized finish, held.

CNC turned 6061-T6 aluminium deflector cones with a true cone angle, radial ports drilled on compound angles and an anodized.

Five-axis machined 6061-T6 aluminium rotary actuator bodies with a through bore, end flanges and ports on compound faces, bored.

304L stainless bearing support blocks with a bored bearing seat to H7, seat and base parallel to 0.02 mm, and clamp-screw flats.

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top