

CNC Turned Stainless Steel Valve Spool
CNC turned 316L stainless valve spools for directional and proportional valves, with land diameters held to ±0.005 mm, groove widths to ±0.02 mm and lands lapped to a 0.005 to 0.012 mm radial clearance in the sleeve. Every groove edge is broken without leaving a burr that would score the bore.
- Land Diameter to 0.01 mm
- Groove Width ±0.02 mm
- Lands Lapped for Fit
- Edge Break 0.05 mm
*Send the sleeve bore with the spool drawing. A spool is only accurate against its sleeve, and a clearance quoted without the bore is a guess that shows up as internal leakage.
Stainless Valve Spool Overview
A spool is the moving part of a valve, and its job is to block flow at one end of the stroke and pass it at the other. That means the land diameter, the groove width and the land spacing all have to be right together, because a 0.01 mm error in land width changes the timing of the valve.
The spool is turned with stock on the lands, grooved to width, then the lands are ground and lapped to the sleeve bore. Groove edges are broken by 0.03 to 0.05 mm so the spool can cross a port without shaving the bore edge, and each spool is fitted to its sleeve before packing.
316L Stainless Bar
316L is used for spools in water, coolant and mild chemical service because the lapped land keeps its finish and does not corrode in a wet bore. It galls less than 400-series steel when it runs in a stainless sleeve.
17-4PH for High Cycle
17-4PH is chosen for spools that cycle millions of times or run at high pressure. After ageing to about 40 HRC the lands resist scoring, and the dimensional change from ageing is allowed for before lapping.
Match the spool and the sleeve in the same material family. A hard spool in a soft sleeve wears the sleeve, and a soft spool in a hard sleeve wears the lands.
Valve Spool Specifications
Turning and lapping data for spools, with the land, groove and clearance values that decide leakage and timing.
| Specification | Machining Data | Specification | Machining Data |
|---|---|---|---|
| Product | Directional Valve Spool | Machining Process | CNC Turning, Grooving, Lapping of Lands |
| Material | 316L / 17-4PH Stainless Bar | Land Diameter Tolerance | ±0.005 mm, Matched to Sleeve |
| Diameter Range | 6 – 30 mm | Groove Width | ±0.02 mm |
| Length Range | 40 – 200 mm | Land Roundness | 0.003 mm |
| Land Count | 2 – 6 Lands on One Spool | Land to Land Coaxiality | 0.005 mm |
| Spool Bore Fit | 0.005 – 0.012 mm Radial Clearance | Surface Finish | Ra 0.2 µm on Lands, Ra 0.8 µm in Grooves |
| Edge Condition | 0.03 – 0.05 mm Break, No Burr in Groove | Straightness | 0.01 mm Over the Spool Length |
| Customization | Land Spacing, Groove Profile, End Thread, Detent Groove | Lead Time | 8 – 11 Days (Sample), 14 – 18 Days (Batch) |
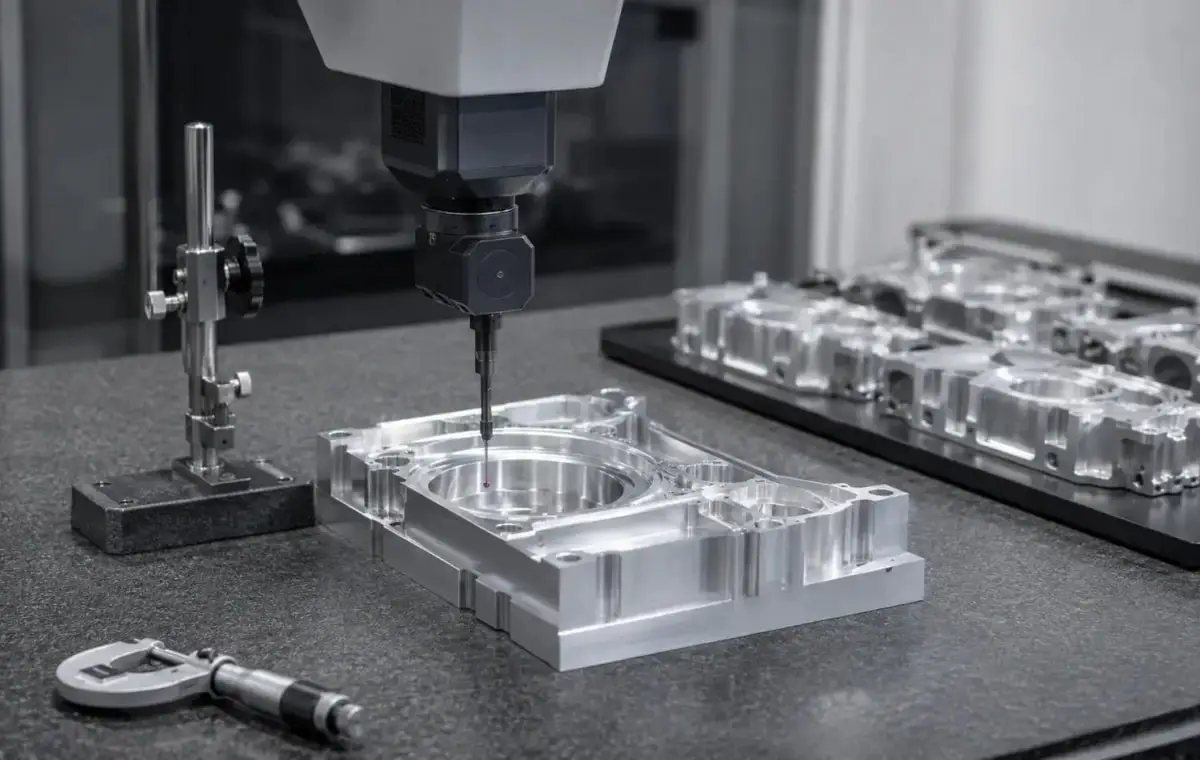
| Inspection | Air Gauge Lands, Optical Groove Width, Roundness, Fit Test | Packing | Sleeved, Oil-Filmed, Individually Boxed |
Key Features of Our Turned Spools
Lands matched to the sleeve, grooves cut to width, edges broken without a burr.
Lands Lapped to the Sleeve
Each spool is lapped against its own sleeve bore, so the radial clearance sits at 0.005 to 0.012 mm and internal leakage is set by design rather than by luck.
Groove Width Held to ±0.02 mm
Groove width is measured optically rather than with a caliper, which keeps the port timing consistent from spool to spool.
Burr-Free Groove Edges
Edges are broken by 0.03 to 0.05 mm with a controlled tool path, so the spool can cross a port without lifting a burr into the clearance.
Fit Tested Before Packing
Every spool is slid through its sleeve by hand and checked for stick-slip, then oil-filmed and sleeved so the lapped surface is not touched in transit.
Need spools matched to your sleeves?
Surface Finishes for Valve Spools
Lapping sets the fit, so any coating is applied before lapping or kept off the lands entirely.
| Finish | Main Purpose | Finish | Main Purpose |
|---|---|---|---|
| As Machined and Lapped | Bare lands where the spool runs in a matched sleeve | Passivation | Removes embedded iron after lapping |
| Electropolishing | Bright lands with a lower friction in the sleeve | Hard Chrome (Selective) | Wear resistance on high-cycle spools |
| Vibratory Polishing | Removes groove burrs before lapping | Oil Film | Corrosion protection in storage and transit |
*Electropolishing removes 2 to 5 µm from a land, which opens the clearance. Spools that are polished are turned 5 µm over size and lapped after polishing.
Put your CNC milling parts into production today
All information and uploads are secure and confidential.
Trusted for Precision CNC Machined Components
Supporting OEM projects with accurate machining, flexible production, and reliable component quality.
Trusted for Precision CNC Milling.
Turning and Lapping Process for Spools
Each land is turned, ground and lapped to its sleeve, so the spool slides without leakage at either end of its stroke.
01. Sleeve and Timing Review
Check the sleeve bore, the land spacing and the port positions against the drawing, and confirm the clearance the valve design requires.
02. Turn With Grinding Stock
Turn the spool with 0.1 mm left on each land, cut the grooves to width and turn the end features in the same cycle.
03. Grind and Lap the Lands
Grind each land to size, then lap to the sleeve bore, checking roundness and clearance as the fit develops rather than at the end.
04. Deburr Grooves and Passivate
Break the groove edges by 0.03 to 0.05 mm, clean ultrasonically and passivate so the lapped surface keeps its corrosion resistance.
05. Fit Test and Pack
Slide each spool through its sleeve, check for stick-slip at both ends of the stroke, then oil-film, sleeve and box individually.
Send the sleeve bore, the port layout and the cycle requirement, and we will quote the spool with the clearance and lapping route set.
Valve Spool FAQs
0.005 to 0.012 mm radial for a hydraulic directional valve, and up to 0.02 mm for pneumatic service. The number is set by the acceptable internal leakage, so it comes from the valve design rather than from a standard table.
Yes. Send the sleeve and the spool is lapped to its actual bore rather than to a nominal size, which is the only way to get a consistent fit on a worn or reworked sleeve.
Optically, on a profile projector or a vision system, because a caliper cannot reach into a groove without a knife edge and even then the reading depends on the operator. Width is held to ±0.02 mm.
A burr on a groove edge scores the sleeve bore as the spool crosses a port, and the score becomes a leak path. The 0.03 to 0.05 mm break removes the burr without changing the timing.
A spool at 0.005 mm clearance will seize on particles larger than the clearance, so filtration is part of the design. For dirty service we recommend 0.012 mm clearance and a hardened land.
Eight to eleven days for a sample including turning, grinding, lapping, passivation and fit test. Batches of 50 to 200 spools run fourteen to eighteen days.
Other CNC Machined Mechanical Components
Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.
Custom CNC machined robot end effector flanges for tool mounting and automation.
Custom Brake Lever CNC Milled components manufactured with precision CNC machining, supporting OEM customization, lightweight.
Custom CNC machined aluminum automotive housings for sensor, actuator and pump assemblies.
Precision CNC machined aluminum indexing rotary tables for automation cells.
Precision CNC machined aluminum connecting plates for robot modules and automation equipment.
Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!