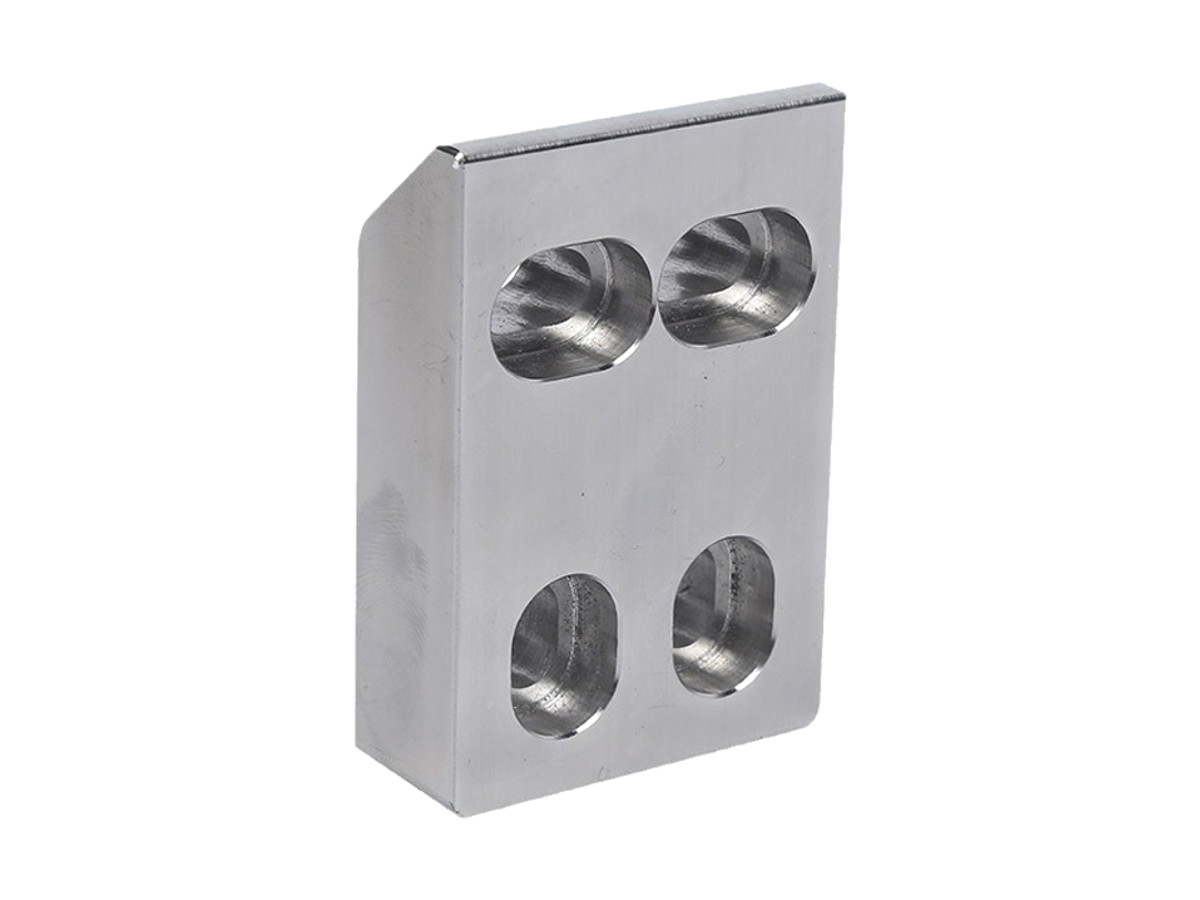
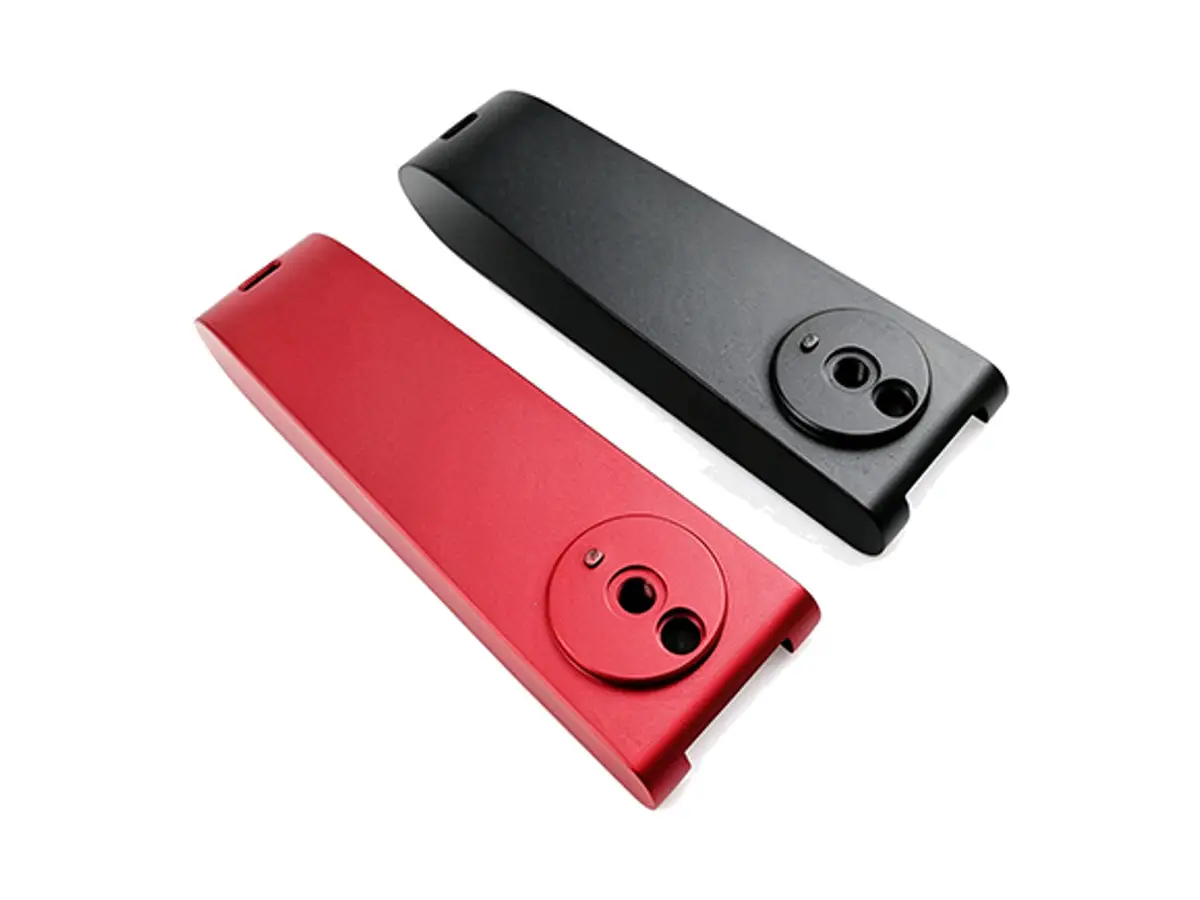
CNC Machined Aluminum Flanged Manifold Housing
Flanged manifold housings machined from 6061-T6, with an H7 bore round to 0.02 mm, a seal groove concentric within 0.03 mm, a flange face square to the bore within 0.03 mm and a bolt circle held to ±0.05 mm. The bore is masked before anodizing so the fit is unchanged.
- Bore H7, Roundness 0.02 mm
- Seal Groove Cut in One Pass
- Flange Face Square to the Bore
- Bolt Circle Within 0.05 mm
*Send the mating flange and the seal drawing. The groove width is set by the O-ring cord you use, and a groove cut 0.1 mm deep will leak no matter how well the faces are machined.
Flanged Manifold Housing Overview
This housing does three jobs at once: it carries a bore for a piston or a spool, it seals against a mating flange and it locates itself on a bolt circle. If the groove is not concentric to the bore, the seal is compressed on one side only.
The block is squared, the flange face is machined, then the bore is roughed, finished and grooved without moving the part. The bolt circle is drilled from the bore axis, and the whole part is checked on the CMM before anodizing.
6061-T6 Aluminium Block
6061-T6 holds a H7 bore well and anodizes to a hard enough surface for a static seal land. It is the default for air and low-pressure hydraulic housings up to 200 mm.
6082-T6 or 7075-T6
6082-T6 is used where the housing is welded to a tank or a pipe run, and 7075-T6 where the wall between the bore and the bolt holes falls under 6 mm and the flange has to resist bolt preload.
A 6 mm wall is the floor for a pressurised housing; below that the bore goes oval when the flange bolts are torqued, even if it was round on the bench.
Flanged Manifold Housing Specifications
Boring and milling data for flanged housings, with the bore, groove and bolt circle values that decide whether the joint seals.
| Specification | Machining Data | Specification | Machining Data |
|---|---|---|---|
| Product | Flanged Manifold Housing / Port Housing | Machining Process | 3-Axis CNC Milling, Boring, Grooving |
| Material | 6061-T6 Aluminium Block | Envelope | Up to 200 × 200 × 120 mm |
| Main Bore | Ø 40 – 110 mm, H7, Roundness 0.02 mm | Bore Finish | Ra 1.6 µm, Ra 0.8 µm on Request |
| Flange Face | Square to the Bore Within 0.03 mm | Flange Size | Square or Round, 120 – 200 mm |
| Seal Groove | Width ±0.03 mm, Depth ±0.02 mm | Groove Concentricity | 0.03 mm to the Bore |
| Bolt Circle | ±0.05 mm, Counterbore Depth ±0.05 mm | Wall Thickness | 6 – 12 mm |
| Side Ports | G1/4 – G1, Square to the Bore 0.1 mm | Drain Boss | Position ±0.1 mm |
| Customization | Side Ports, Drain Boss, Lifting Eyes, O-Ring Grooves | Lead Time | 6 – 8 Days Sample, 12 – 18 Days Batch |
| Inspection | Bore Air Gauge, CMM Flange Squareness, Groove Pin Gauge | Packing | Bore Plug, Foam Cradle, Crate |
Key Features of Our Flanged Housings
Bore, groove and flange face from one set-up, checked before coating.
Bore and Groove in One Set-up
The groove is cut with the boring bar still in the same datum, so it stays concentric to the bore within 0.03 mm and the seal compresses evenly.
Flange Face Square to the Bore
The face is faced after boring, which keeps it square within 0.03 mm and stops the housing cocking on its gasket when the bolts are tightened.
Bolt Circle From the Bore Axis
Holes are positioned from the bore centreline rather than the outside of the block, so a replacement housing lines up with the pipework without reaming.
Bore Plugged for Anodizing
The bore is masked with a plug before coating so the H7 fit is untouched, and it is air gauged again after anodizing before packing.
Housing that has to seal on a machined flange?
Surface Finishes for Flanged Housings
The outside is visible, the bore is a fit and the groove is a seal seat, so only the outside gets the full coating.
| Finish | Main Purpose | Finish | Main Purpose |
|---|---|---|---|
| Clear Anodizing | Corrosion protection without hiding the machined faces | Black Anodizing | Visible equipment finish |
| Masked Bore and Groove | Keeps the H7 fit and the groove depth after coating | Bead Blasting | Even matte on the outside faces |
| Chromate Conversion | Conductive finish where the housing is earthed | Laser Marking | Bore size and assembly orientation |
| Anodizing Build | 10 – 20 µm, Sealed | Hydrostatic Test | 1.5 × Working Pressure, 10 min |
| Bore Plug | Fitted During Coating | Face Protection | Taped Flange Face for Shipping |
| Vapour Blasting | Satin on the Outside Only | Assembly Oil | Light Film in the Bore |
*Anodizing 10 µm per surface will close a H7 bore by 20 µm and change the squeeze on the seal. Bores and grooves are plugged, or machined undersize and finished after coating on request.
Put your CNC milling parts into production today
All information and uploads are secure and confidential.
Trusted for Precision CNC Machined Components
Supporting OEM projects with accurate machining, flexible production, and reliable component quality.
Trusted for Precision CNC Milling.
Machining Process for Flanged Housings
The bore, the seal groove and the flange face are cut in one set-up, so the groove stays concentric to the bore instead of following the flange.
01. Flange and Seal Review
Check the mating flange, the O-ring cord diameter and the bolt circle, then set the groove width and depth from the seal datasheet.
02. Square and Face the Block
Machine the block square and face the flange side first, because the bore and the groove are both called from that face.
03. Rough and Finish Bore
Drill, rough bore and finish bore to H7, checking diameter at three depths with an air gauge before the tool is withdrawn.
04. Cut Groove and Bolt Circle
Cut the seal groove with a form tool in a single pass, then drill and counterbore the bolt circle from the bore axis.
05. Inspect, Mask and Anodize
CMM the flange squareness and groove concentricity, plug the bore, anodize, then re-gauge the bore and cap the ports.
Send the mating flange and the seal you use, and we will quote a housing with the bore, groove and bolt circle cut from one datum.
Flanged Manifold Housing FAQs
0.03 mm, because both are cut without unclamping. A groove that follows the outside of the block instead of the bore will pinch the seal on one side and weep on the other.
Ra 1.6 µm as standard and Ra 0.8 µm for a sliding spool or a lip seal. Below Ra 0.4 µm the surface holds no oil film and a lip seal will run dry.
Yes, on request the bore is left 40 µm undersize, the housing is anodized and the bore is finish bored afterwards. This suits bores that must stay conductive or carry a sliding fit.
0.05 mm across the seal face. A face that is dished by 0.1 mm will hold on the bolts but leak between them, which is the hardest leak to find.
Yes, a hydrostatic test at 1.5 times working pressure for 10 minutes on request, with the ports blanked. Air testing is available for housings that will not see liquid.
8 mm for a bore up to 80 mm at 1 MPa, and 12 mm where the housing is also a structural mount. Thinner walls go oval under bolt preload before they burst under pressure.
Other CNC Machined Mechanical Components
Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.
CNC machined 316L stainless steel pump connector plates with a lapped seal face, a bored port and a bolt pattern within 0.03 mm,.
316L stainless fluid manifold blocks machined from solid with flat port faces to 0.02 mm, drilled galleries cleared by borescope.
Five-axis milled aluminium curved sensor brackets with swept mounting pads, blended fillets and 0.03 mm pad flatness for robot.
Precision CNC machined aluminum robot joint housings for arm segments and joint modules.
Precision CNC machined aluminum robot joint housing flanges.
Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!