

Home / CNC-Machining / CNC Milling / CNC Machined Aluminium Bracket and Base Set
CNC machined 6061-T6 aluminium bracket, base plate and link arm set

CNC Machined Aluminium Bracket and Base Set

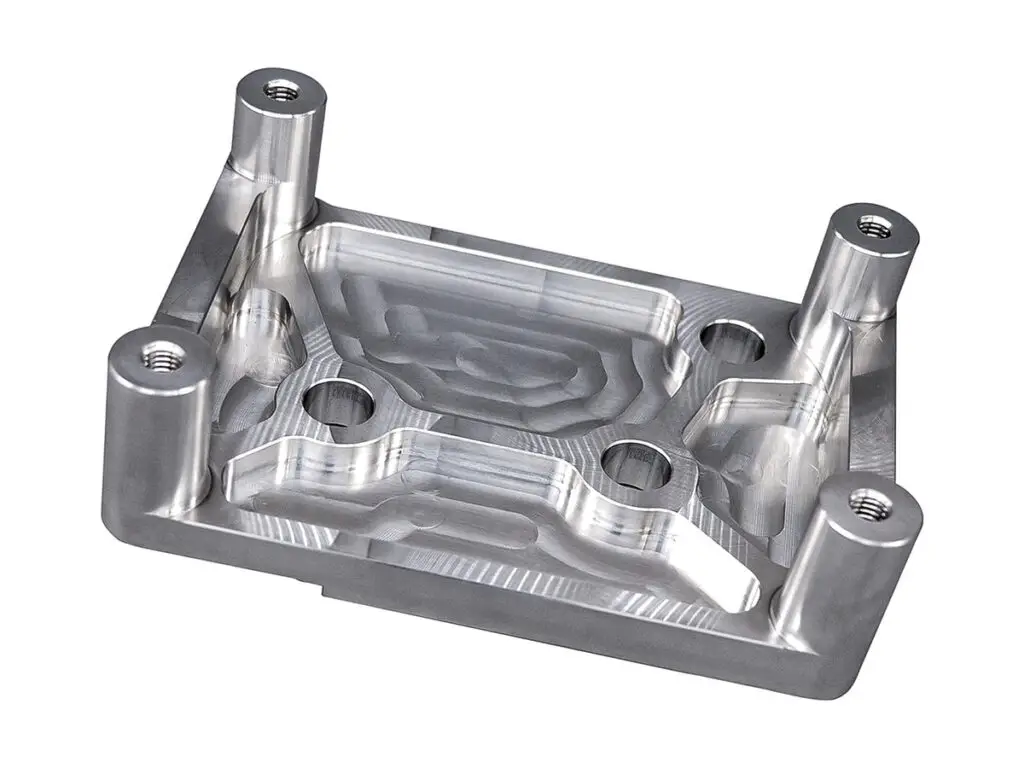
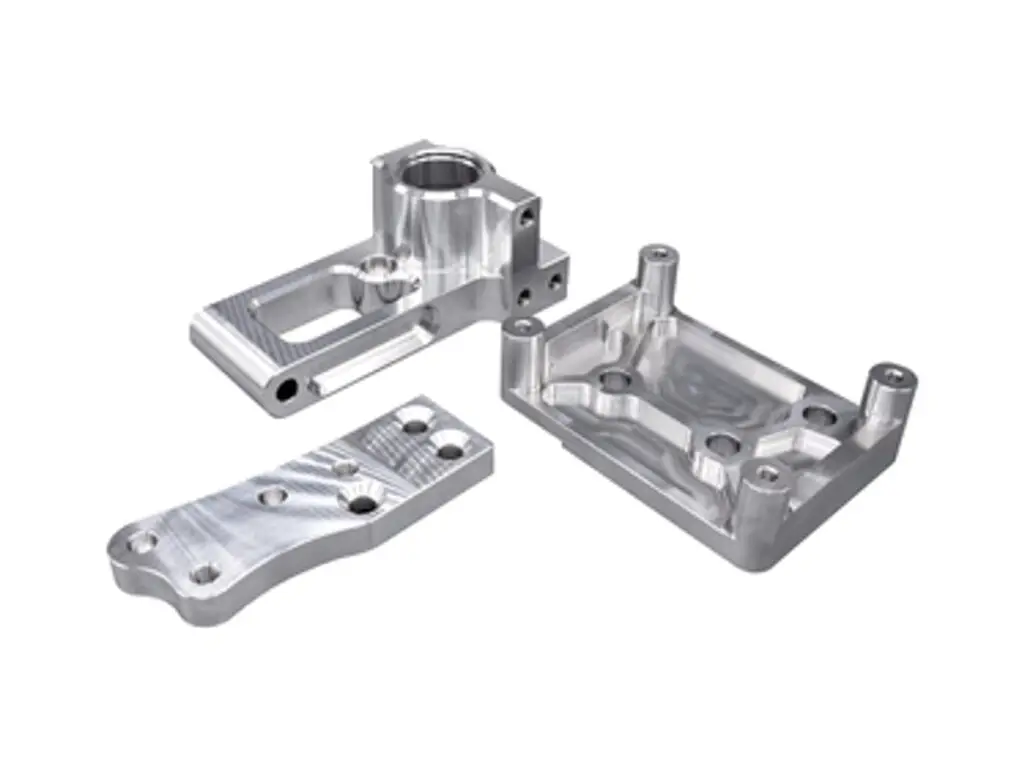
Bracket sets machined from 6061-T6: a 90 × 60 × 45 mm mounting bracket with a Ø26 H7 bore, a 120 × 80 × 18 mm base plate with a 12 mm pocket, and an 8 mm link arm. All three are cut from the same billet, numbered as a set and checked together so the bores stay coaxial within 0.03 mm.

*Send the assembly drawing, not just the individual parts. The stack-up between the bracket bore and the base pocket is what decides whether the arm needs a shim, and that is set at the set level.

Aluminium Bracket Set Overview

A bracket set is only as good as the relationship between its parts. Individually they can all be within tolerance, yet the assembly will not line up if the bracket bore and the base pocket were cut on different datums. Machining them as a numbered set removes that risk.

All three parts are cut from one billet run, the bracket bore is bored in a single clamping, the base pocket is milled with a 0.3 mm finish allowance and the link is profiled from 8 mm plate. The set is trial-assembled on a surface plate before anodizing and the assembly is photographed with the set number.

Workshop production of a stainless steel stepped axle pin
6061-T6 aluminium flat plate stock for CNC milling

6061-T6 Aluminium

6061-T6 gives a stiff bracket at 610 g for the set and anodizes evenly across three parts of different section thickness.

7075-T6 aluminium billet block stock for CNC milling

6082-T6 or 7075-T6

6082-T6 is used when the bracket is welded into a frame, and 7075-T6 is chosen when the link arm carries a reversing load and needs higher fatigue strength.

A pocket floor thinner than 4 mm will drum under clamp load and throw the bore alignment out; the floor is kept at 6 mm under the bracket seat.

Bracket Set Specifications

Set-level values: bore, pocket, matching and the assembly check.

SpecificationMachining DataSpecificationMachining Data
ProductBracket, Base Plate and Link ArmProcess3-Axis CNC Milling, Boring
Material6061-T6 AluminiumBracket Envelope90 × 60 × 45 mm
Base Envelope120 × 80 × 18 mmBracket BoreØ26 H7, ±0.01 mm
Pocket Depth12 mm ±0.05 mmLink Thickness8 mm ±0.05 mm
Squareness0.03 mm Over 100 mmMounting Holes6 × Ø6.6, ±0.05 mm
Set MatchingBores Coaxial Within 0.03 mmWeightApprox. 610 g per Set
Edge Break0.4 mm on Handling EdgesAssemblySupplied as a Numbered Set
InspectionCMM Set Check, Bore GaugeBatch Size10 to 500 Sets
FinishClear Anodizing or As-MachinedDrawing FormatSTEP, DXF, PDF

Machined as a Set, Checked as a Set

One billet run, one datum, one set number.

One Billet Run for All Three Parts

Cutting the bracket, base and link from the same run means the same heat treatment and the same residual stress, so the set does not move differently after anodizing.

Bore and Pocket on One Datum

The bracket bore and the base pocket are generated from the same datum edge, which is what keeps the arm coaxial within 0.03 mm without a shim at assembly.

Trial Assembly Before Coating

The three parts are assembled on a surface plate with the real fasteners and checked for fit before anodizing, so any interference is corrected in bare aluminium.

Set Number on Every Part

Each part carries the set number, which lets a replacement bracket be matched to an existing base instead of replacing the whole assembly.

Assembly that has to line up first time?

Surface Finishes for Bracket Sets

One finish across three parts, with the bores and seat faces masked.

FinishMain PurposeFinishMain Purpose
Clear AnodizingGeneral protection, machined lookBlack AnodizingMachine covers and optical mounts
Hard AnodizingWear face on the link armBead BlastingEven matte before coating
Masked BoreBare bore for a bearing or bushChromate ConversionConductive set for earthing
Laser MarkingSet number on all three partsDeburr OnlySets that will be painted later
Ultrasonic CleanChip removal from pocketsSet BaggingThree parts kept together
Colour MatchKeeps the set in one shadeProtective WrapNo contact marks in transit

*If the three parts are anodized in separate tank loads the colour will not match; the set is always coated together in one load.

logo

Put your CNC milling parts into production today

All information and uploads are secure and confidential.

Trusted for Precision CNC Machined Components

Supporting OEM projects with accurate machining, flexible production, and reliable component quality.

Mechanical Equipment Customer
The three parts lined up on the surface plate with no shim, which is why we bought the set.

Industrial Components Buyer
Bore and pocket were coaxial as quoted, and the arm moves without binding.

Equipment Manufacturer
The set number on all three parts makes spare ordering straightforward.

OEM Customer
OEM Customer
Anodizing is the same shade on every part, including the thin link.

Automation Industry Customer
The customized machining solution provided the dimensional accuracy required for our rotating equipment components.

Trusted for Precision CNC Milling.

How We Machine a Bracket Set

The bracket bore and the base pocket are cut from the same billet run and numbered as a set, so the arm lines up without a shim on assembly.

01. Assembly and Stack-up Review

Read the assembly drawing, not just the part drawings, and check the stack-up between the bracket bore, the base pocket and the link thickness.

02. Cut the Billet Run

Saw the bracket, base and link blanks from one billet, mark the set number on each and keep them together through the whole process.

03. Machine Bracket and Base

Bore the Ø26 H7 bracket bore, mill the 12 mm base pocket to ±0.05 mm and drill the six mounting holes in the same datum scheme.

04. Profile the Link and Trial Fit

Profile the 8 mm link arm, deburr all three parts and assemble the set on a surface plate to check the bore alignment before coating.

05. Anodize Together and Certify

Anodize the set in one tank load, mask the bores, then re-check the assembly and issue the set inspection sheet.

Send the assembly drawing and the fastener callouts, and we will quote a numbered set with the bracket bore and base pocket machined on one datum.

Bracket Set FAQs

No, but the price and the alignment guarantee assume the set. A single bracket is quoted from the part drawing alone and carries a part tolerance, not a set tolerance.

The three parts are assembled on a surface plate with the specified fasteners and the bore alignment is measured with a pin and a dial indicator. The result is recorded against the set number.

Yes, but they are then coated in separate loads and we cannot guarantee an exact colour match between them.

We keep the set record, so a replacement can be machined to the original set datum and marked with the same number.

The base pocket is 12 mm deep as drawn. If a bearing needs a deeper seat, the pocket is machined to the bearing drawing and the floor thickness is re-checked.

Yes, with the fasteners torqued to your value and the assembly marked, which is common for cells that install the unit as one item.

Other CNC Machined Mechanical Components

Explore additional precision CNC machined components manufactured for OEM applications and customized production needs.

Five-axis CNC machined 6082-T6 aluminium manifold plates with cross-drilled galleries, spotfaced port faces and ports on five.

CNC machined 7075-T6 aluminium fork slider legs with a honed bore, machined axle slots and brake caliper lugs, held to ±0.03 mm.

CNC machined 316L stainless hinge blocks with twin knuckle bores, a square mounting face and a matched pin bore, holding knuckle.

CNC turned 316L stainless cylinder cups with a thin uniform wall, a flat closed end and a bore to H8, machined from solid bar and.

CNC machined 6061-T6 aluminium servo actuator housings with a bored bearing register, ribbed walls and a machined gasket face,.

Get high‑quality machined parts in as fast as 4 days with our expanded automated CNC milling!

Scroll to Top